The Material That Keeps Everything From Sticking Together
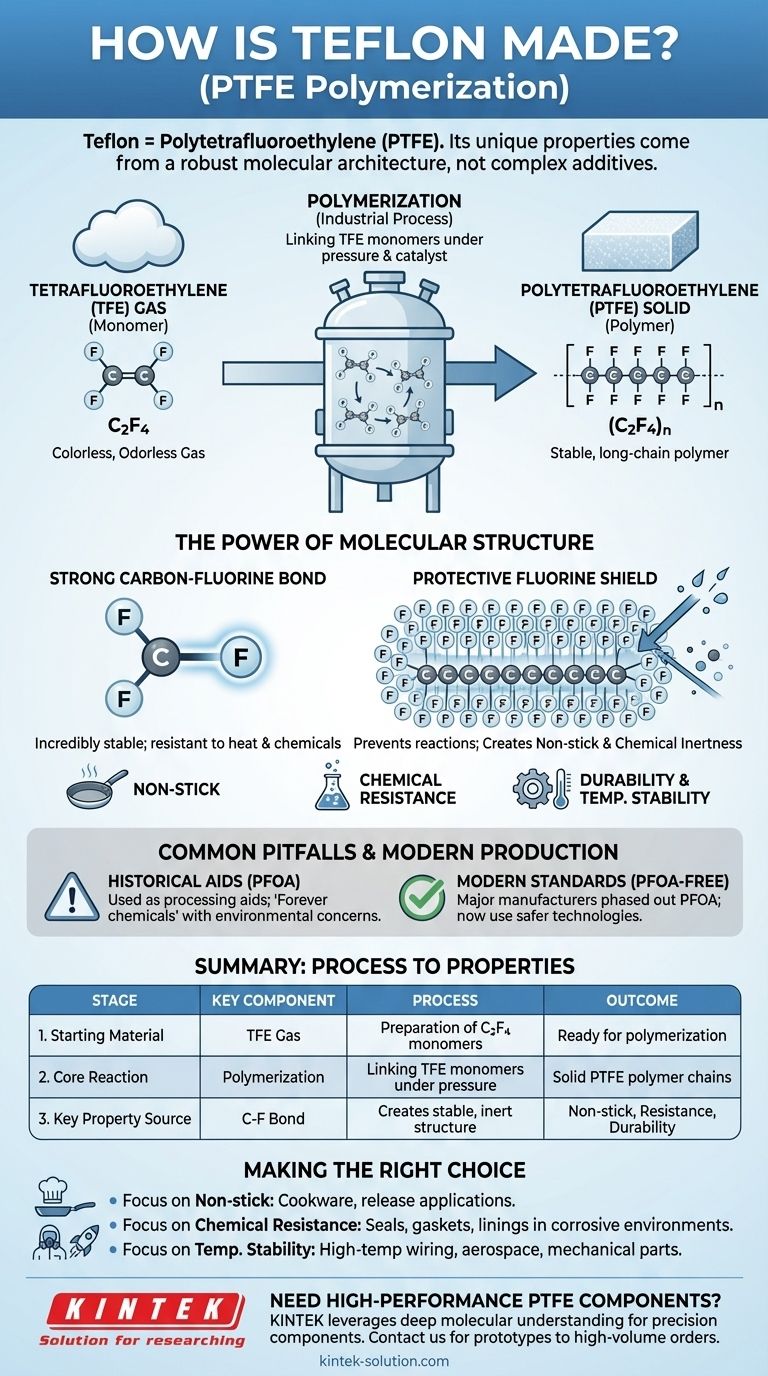
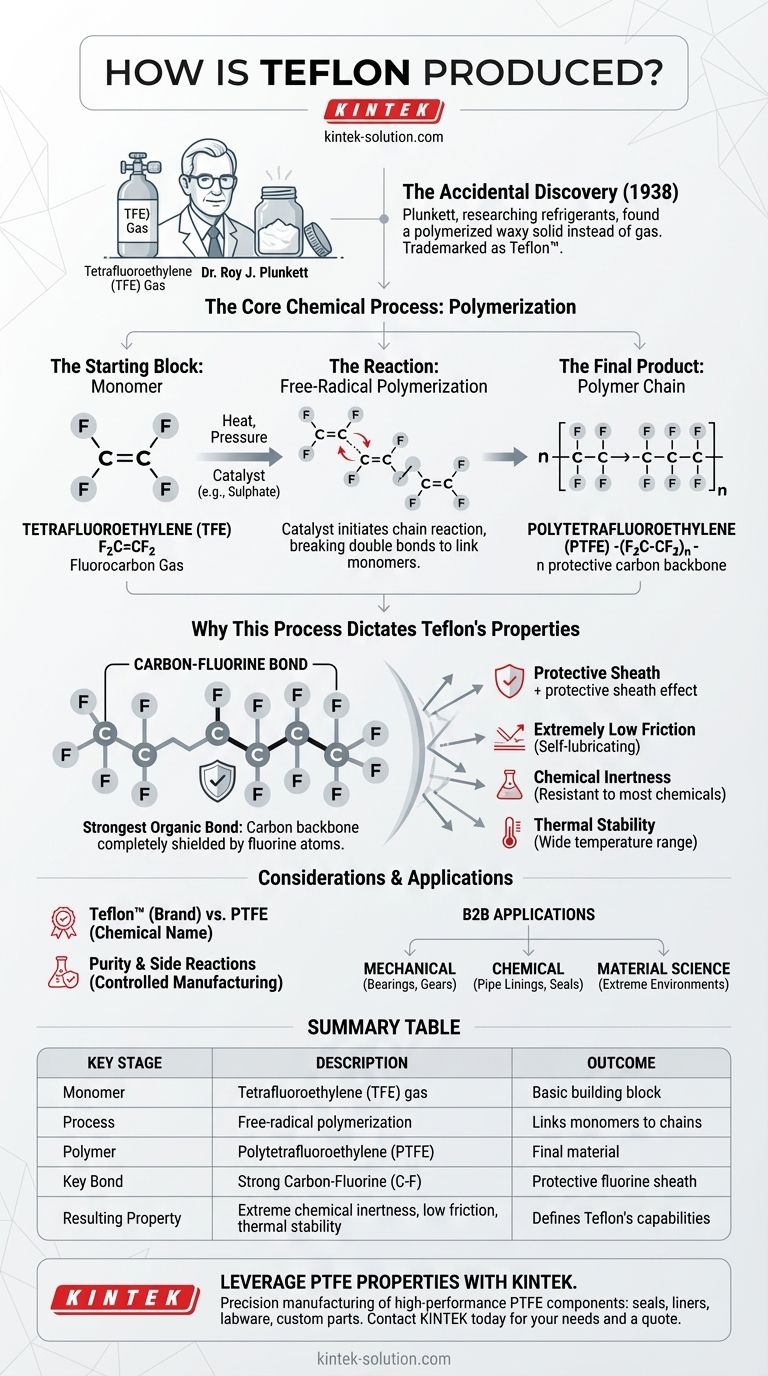
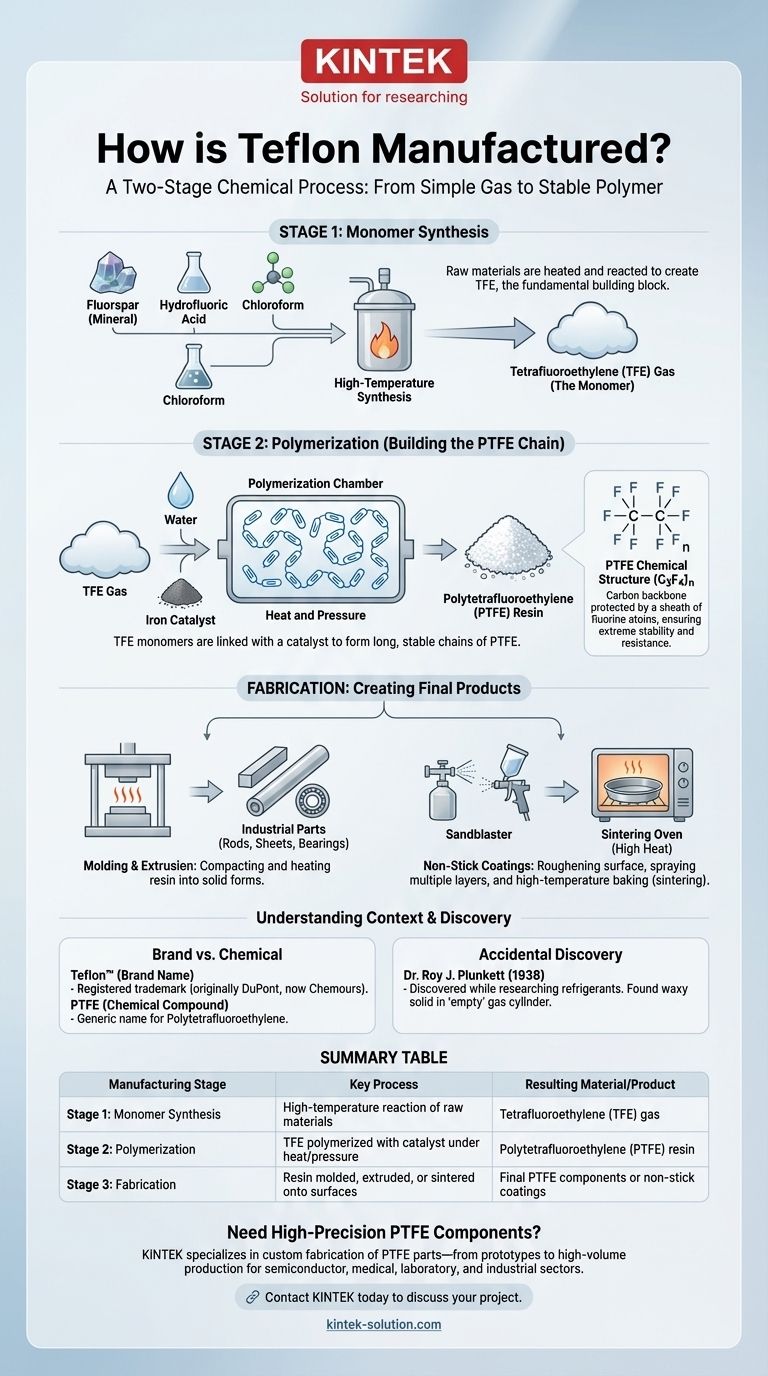
Most people have never heard of polytetrafluoroethylene by name, but they interact with it dozens of times a day. The stuff shows up as a non-stick coating on cookware, a sealant in plumbing, a lining in wire insulation, and a component in medical devices. It does all of these jobs because fluorine atoms wrap around a carbon backbone so tightly that virtually nothing else wants to bond to it. That chemical is what makes it useful and what makes it a pain to work with. When I first ran into this material in a manufacturing setting, I was trying to solve a problem where food residue kept building up on conveyor belts in a processing plant. Standard rubber gaskets and steel surfaces were failing within weeks. The replacement was straightforward on paper — coat the contact surfaces with PTFE and you're done. It wasn't straightforward in practice. The first issue is that raw PTFE doesn't adhere to anything. It has one of the lowest coefficients of friction of any solid material, which is exactly the point, but it also means you can't just paint it on and expect it to stay. The standard workaround is sintering. You mix the PTFE powder with a binder, apply it to the substrate, and then heat the whole thing to around 370 degrees Celsius. The binder burns off and the polymer fuses into a continuous layer. I've seen this process mess up tolerances by half a millimeter if you don't account for shrinkage, which happens in about 3 to 4 percent during cooling. Factor that in or your part won't fit.
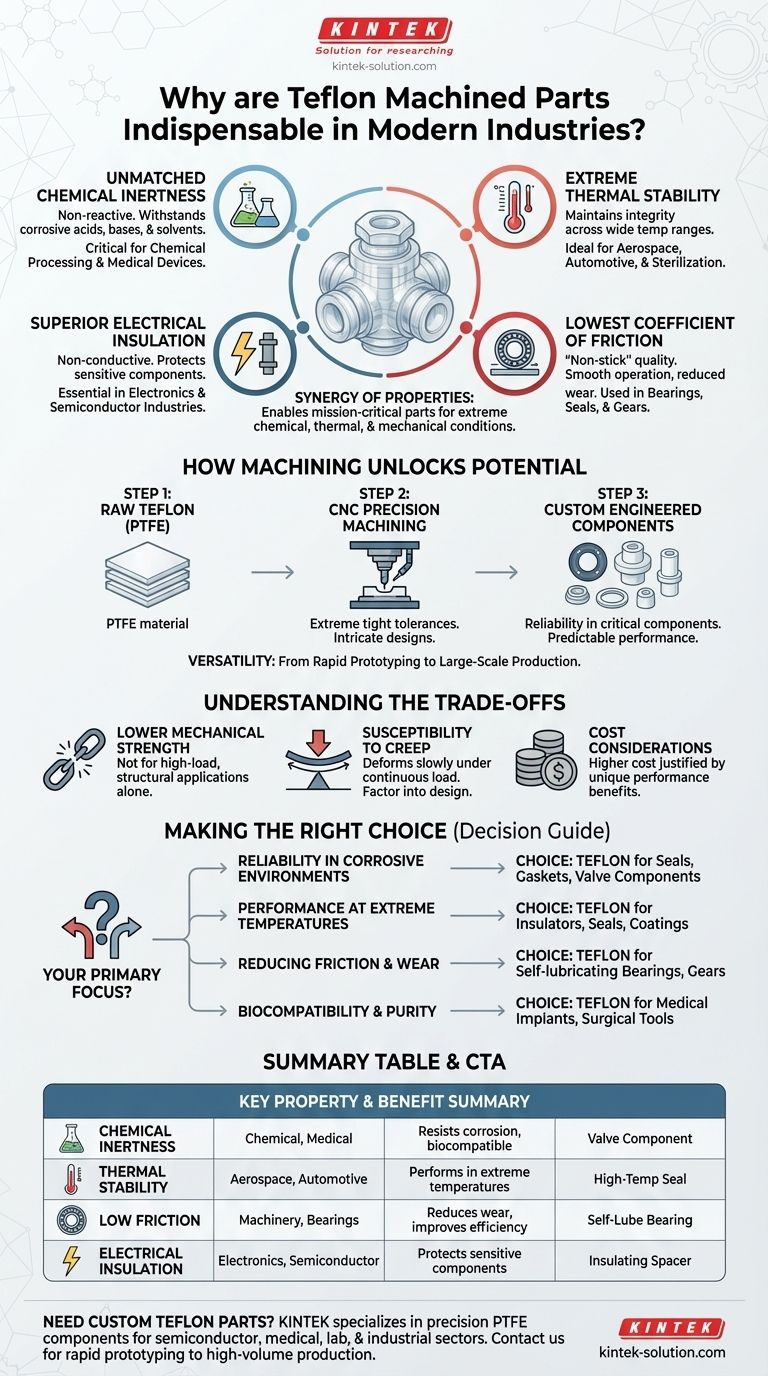
Another thing nobody warns you about is cold flow. PTFE is viscoelastic, which means under sustained load it will slowly deform over time. I had a seal that looked fine when installed and passed inspection, then three months later it had flattened enough to leak because the bolted joint was holding constant pressure. The fix was switching to a filled PTFE compound — bronze or carbon black mixed into the base polymer reduces cold flow significantly. You trade a little non-stick performance for structural stability, and that trade-off is usually worth it. There are scenarios where this material simply won't work. At temperatures above 260 degrees Celsius, it starts breaking down and releasing decomposition products that are hazardous to inhale. Above 350, the degradation accelerates rapidly. If your process runs hot, you need to look at alternatives like PFA or FEP, which have higher thermal limits but cost more and are harder to fabricate. Another hard limit is UV exposure over long periods — outdoor applications without protective coatings will degrade within a couple years. I learned that the hard way on an exterior wiring harness that became brittle and cracked after two summers. The fabrication side has its own quirks. Machining solid PTFE stock produces chips that are notoriously gummy and difficult to clear from deep holes. Use sharp tools, slow feed rates, and plenty of air blast. Attempting to weld it conventionally doesn't work because it doesn't melt the way thermoplastics like polypropylene do — it goes straight from solid to a highly viscous melt without a true liquid phase. Roto-molding and ram extrusion are the go-to methods for complex shapes.
For anyone specifying this material for a project, the practical advice is simple: know your temperature range, account for cold flow under load, factor in shrinkage during forming, and don't assume the coating will stick to your substrate without proper surface preparation. Sandblast the bonding surface to about 2 microinches RMS, apply a primer designed for fluoropolymers, and then do the sinter cycle. Skip the primer and you'll spend more time reworking failed bonds than you would have spent doing it right the first time.
Get the Full Details