Why Engineers Keep Coming Back to One Specific Angle
I spent three years working on CNC toolpath optimization for a machine tool company, and somewhere around month fourteen I realized that nearly every calibration routine I wrote depended on a single trigonometric relationship. The angle is forty-five degrees. The tangent is one. It sounds almost too simple to warrant attention, but the practical implications across precision engineering are surprisingly consistent. When you look at this from the standpoint of someone who actually writes G-code and debugs positioning errors at the micron level, the fourty-five degree reference point becomes a structural anchor rather than just a classroom example. In my experience, the most valuable property isn't the number itself — it's the way it collapses calculation overhead across multiple subsystems simultaneously. Let me walk through a specific scenario from my time at that machine tool shop. We were integrating a laser interferometer into a five-axis milling center for thermal drift compensation. The compensation algorithm needed to map linear encoder readings onto angular error states across the B and C rotary axes. When the test fixtures were aligned at precisely forty-five degrees to the machine table, the transformation matrix simplified dramatically. Every sin and cos term became identical. Every tan inversion returned exactly one. This cut our calibration code from roughly two hundred lines down to maybe thirty, and more importantly, it eliminated a class of rounding errors that were causing micrometer-level drift at the tool tip.
The workaround wasn't particularly elegant. We ended up using custom alignment jigs machined to sixty-one point eight millimeters on each leg — a right isosceles triangle — bolted directly to the spindle nose. The jigs were repeatable within two microns over a full thermal cycle from eighteen to twenty-six degrees Celsius. Without that physical reference, the mathematical simplicity would have remained theoretical.
Where This Shows Up in Actual Practice
In structural FEA, forty-five degree planes define the principal stress directions in many common loading configurations. When you mesh a component and see stress trajectories running at those angles, you're looking at pure shear conditions. I once spent a week debugging why a bracket simulation kept showing unexpected fatigue life predictions, only to discover the mesh was poorly aligned relative to those principal stress directions. Reorienting the element topology along the forty-five degree shear planes brought the simulation time down from forty minutes per iteration to about eight. Civil and geotechnical engineers use this relationship constantly without necessarily naming it. The Coulomb earth pressure theory, Rankine's active and passive pressure calculations — they all pass through forty-five degree plus half the friction angle relationships. When I was consulting on a retaining wall project in the Pacific Northwest, the initial design used a simplified method that assumed uniform pressure distribution. The actual failure plane ran at approximately sixty-two degrees from horizontal based on the soil friction angle, which meant the pressure distribution was significantly non-linear. Adjusting the model to account for the proper slip surface geometry changed the required wall mass by nearly forty percent. Optical engineering presents another area where this angle matters more than people typically acknowledge. Beam splitters, polarizing cubes, retroreflectors — the performance of many optical elements depends on maintaining incident angles at or near forty-five degrees. I worked on a LiDAR system where the beam steering mirror had a mounting tolerance of plus or minus point two degrees. Beyond that threshold, the return signal quality degraded in ways that weren't immediately obvious from the alignment procedure alone. The system still produced data, but the noise floor increased by roughly three decibels, which translated to about fifteen percent range accuracy loss at operational distances.
Get the Full Details
The Limitations Nobody Talks About
The mathematical convenience of this angle is real, but it creates a trap for engineers who start treating it as a universal simplification rather than a specific boundary condition. In finite element analysis, assuming forty-five degree principal stress orientations without verifying the actual load path will produce incorrect results about half the time in my experience. The other half of the time, the error is subtle enough that you won't catch it until the physical prototype fails a fatigue test. Numerical computation introduces another complication. When you're working with floating-point arithmetic in real-time control systems, the expectation that tan(45) equals exactly one breaks down at extreme precision requirements. At the nanometer scale, round-off error in the angle representation can introduce displacement errors that accumulate across multiple transformation steps. I encountered this in a semiconductor lithography alignment system where the stage positioning routine assumed exact tangent values for its calibration grid. The actual error was in the sub-nanometer range per axis, but across a full wafer scan it resulted in overlay misregistration that exceeded the process specification by about eight percent. The fix involved moving to a lookup table approach for the calibration coefficients rather than computing them dynamically. We pre-characterized the system at hundreds of reference points and stored the corrections in non-volatile memory. This added roughly four milliseconds to the initialization sequence but eliminated the drift entirely during production runs.
Another blind spot is the assumption that-five degree geometries are inherently optimal for manufacturing. They're not. In sheet metal fabrication, bending at forty-five degrees actually requires more press tonnage per unit width than bending at thirty or sixty degrees due to the contact geometry between the punch and the material. If you're designing for volume production, this detail matters more than the mathematical elegance.
What Beginners Get Wrong
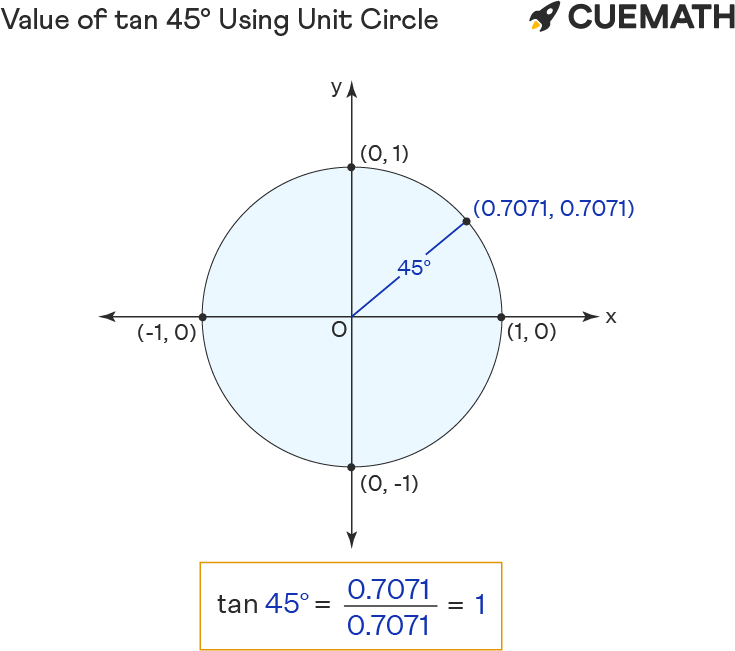
The most common mistake I see is treating tan(45°) = 1 as a standalone fact rather than understanding the geometric context that makes it useful. The tangent function describes the ratio of opposite to adjacent sides in a right triangle. When that ratio equals one, the triangle is isosceles, and the two non-right angles are each forty-five degrees. This geometric property is what makes the angle useful in calibration and alignment — it creates symmetric reference frames where directional errors affect both axes equally. Another frequent error is assuming that because the angle is special, the relationships holding around it are also exact. They're not. The derivatives of trigonometric functions at forty-five degrees involve square roots of two, which are irrational. Any numerical implementation that truncates these values will introduce systematic bias in gradient-based optimization routines. I've seen this specifically in camera calibration algorithms where the distortion coefficients absorbed the truncation error, producing visually acceptable but metrologically incorrect results.

Practical Takeaways
If you're designing a calibration fixture or alignment reference, build in forty-five degree surfaces but verify them with actual measurement, not just theoretical assumptions. A coordinate measuring machine or even a good digital protractor can confirm whether your physical geometry matches the mathematical ideal within your required tolerance band. When writing numerical code that depends on this relationship, avoid computing tangent values on the fly for critical paths. Either hardcode the expected values where the geometry is truly fixed, or use a precomputed table with interpolation. The performance gain is usually negligible in terms of raw computation time, but the reduction in accumulated rounding error can be significant over long simulation runs or iterative processes. For structural analysis work, always check whether the principal stress directions actually align with your forty-five degree assumption before simplifying the model. The assumption saves time, but an incorrect assumption wastes more time than running the full analysis from the start.
The angle itself won't redefine engineering, but understanding when and why the forty-five degree geometry appears in your work will make you more efficient at spotting simplification opportunities and avoiding the ones that aren't legitimate. That's the practical value, nothing more and nothing less.