Why Your Suspensions Keep Settling (And What Actually Fixes It)
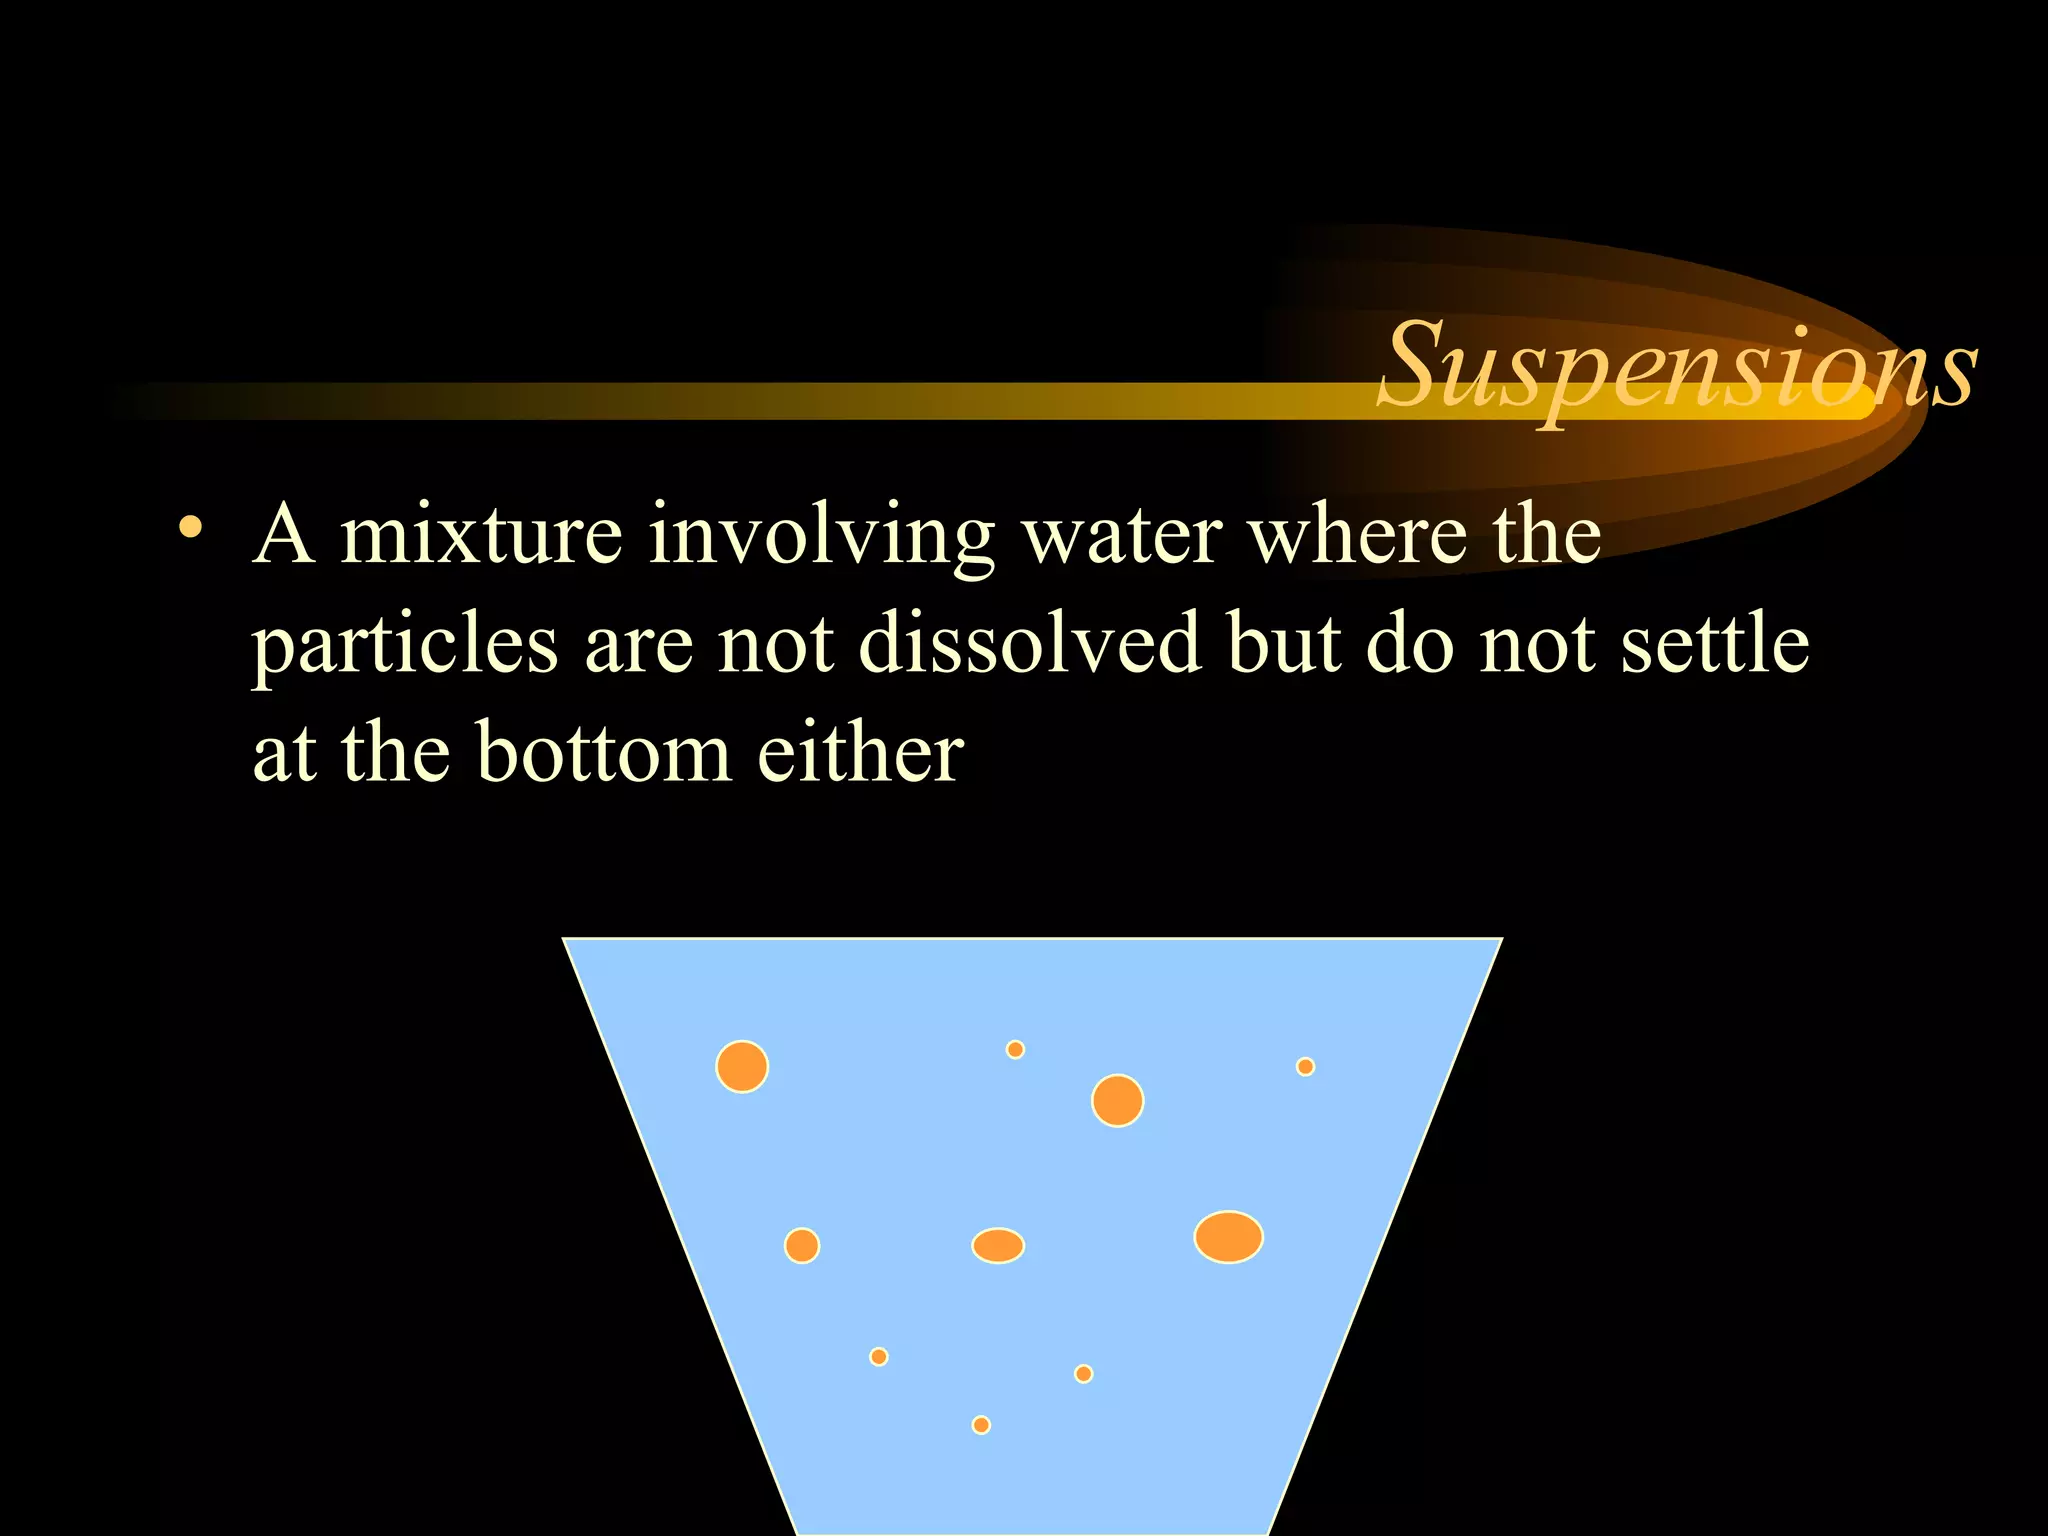
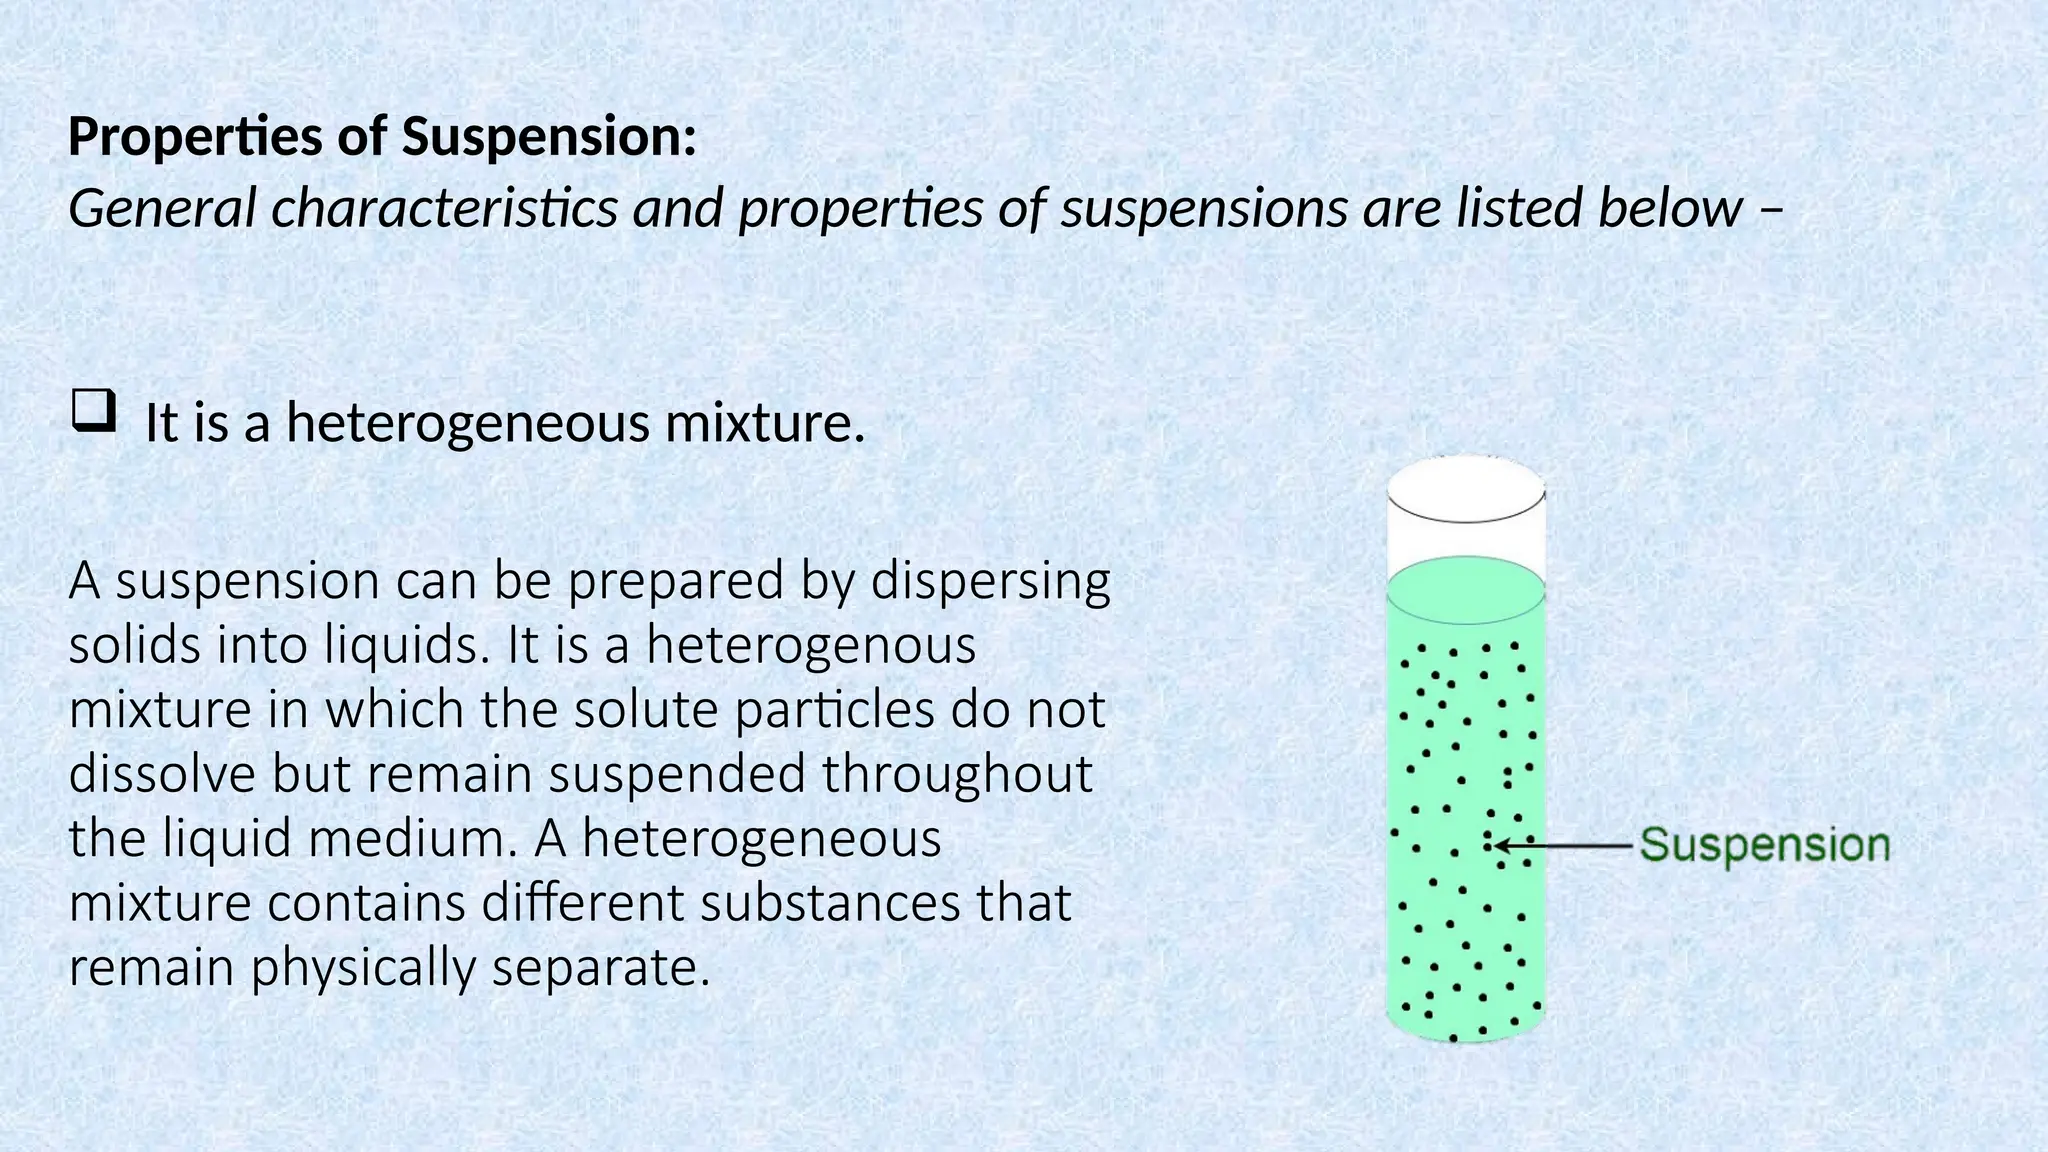
Suspensions look fine when you first make them. You stir in the powder, the liquid goes opaque, everything seems normal. Then you leave it on the shelf for three days and you get a rock-hard cake at the bottom that won't re-disperse no matter how hard you shake it. This is the universal suspension problem. The difference between a product that stays stable and one that becomes a science experiment in caking comes down to understanding what's actually happening at the particle level. A suspension is simply a heterogeneous mixture where solid particles are distributed throughout a liquid medium but aren't dissolved. The particles are large enough to scatter light, which is why suspensions look cloudy or opaque. Unlike true solutions, the solids in a suspension will eventually settle under gravity. That's not a defect, it's physics. Stokes' Law describes the settling velocity: it depends on particle size squared, the density difference between the solid and the liquid, and the viscosity of the medium. Everything else you do is trying to manipulate those variables. Here's the thing most tutorials don't tell you clearly enough. Particle size distribution matters way more than average particle size. A narrow distribution where every particle is roughly the same size tends to settle faster than a broader distribution. The small particles slip into the gaps between the large ones and pack densely. That dense packing creates a continuous solid network that becomes a hard cake. When you have a range of sizes, the smaller particles fill voids between larger ones during settling, but they don't form that rigid interconnected structure as easily. The result is a looser sediment that's far easier to re-disperse.
I spent about six months dealing with a particular oral suspension formulation where the active ingredient kept caking no matter what we did. We tried increasing the viscosity with CMC-Na, we tried different surfactants, we tried changing the pH to move away from the isoelectric point. Nothing worked consistently. The breakthrough came when I realized we were using a single-mill version of our API and it had an extremely narrow particle size distribution around 45 microns. Once we switched to a dual-mill approach that gave us a bimodal distribution with modes around 20 and 60 microns, the sediment became fluffy and re-dispersed completely with a simple shake. The viscosity was actually lower in the final product because we'd reduced the thickener load. It felt counter-intuitive at the time but it made perfect sense once I stopped thinking about it as just "make the liquid thicker" and started thinking about packing geometry.
The Zeta Potential Trap
Zeta potential is one of those measurements everyone talks about when discussing suspension stability but rarely understands correctly. A high absolute zeta potential value above 30 mV generally indicates good electrostatic repulsion between particles. The assumption is that if your zeta potential is high, your suspension will be stable. This is mostly true in simple aqueous systems but it falls apart quickly in real formulations. The problem is that zeta potential only measures electrostatic stabilization. It says nothing about steric stabilization, which is often the dominant mechanism in commercial products. You can have a zeta potential of only 15 mV and a perfectly stable suspension if you've got adequate steric barriers from polymers or surfactants adsorbed onto the particle surfaces. Conversely, you can have a zeta potential of 45 mV and still get rapid flocculation if the ionic strength of your medium is high enough to compress the electrical double layer. Flocculated versus deflocculated suspensions represent another area where people get tripped up. A deflocculated suspension has well-separated individual particles that settle slowly and form a dense compact cake. A flocculated suspension has loose aggregates that settle faster but form a voluminous loose sediment that redisperses easily. For most practical purposes, especially in pharmaceutical and food suspensions, you actually want a controlled flocculated system. The apparent paradox is that accepting faster settling gives you better long-term stability because you avoid caking entirely.
Get the Full Details

Practical Stabilization Strategies That Actually Work
Wetting agents are non-negotiable for hydrophobic particles. If your solid doesn't wet properly, air gets trapped on the particle surfaces and you get inconsistent dispersion no matter how much energy you put into mixing. Sodium lauryl sulfate at 0.1 to 0.5 percent is a standard starting point. Polysorbate 80 works well for many applications too. The key is to pre-mix the wetting agent with your powder before adding the bulk liquid. Skip this step and you'll spend twice as long getting acceptable dispersion quality. Viscosity modifiers are the most obvious tool and also the most misused. Adding more thickener does increase stability by reducing settling velocity according to Stokes' Law. But there's a practical limit. Once your suspension becomes so viscous that it's unusable, you've solved one problem and created another. The smarter approach is using rheology modifiers that provide yield stress. These materials behave like a solid below a certain stress threshold and flow like a liquid above it. This means your particles stay suspended at rest but the product still pours or spreads when you apply force. Xanthan gum and fumed silica are common choices here. Density matching sounds like the obvious solution. If the solid and liquid have the same density, particles won't settle at all. In practice this is extremely difficult to achieve and maintain. You have to account for temperature variations which change liquid density. You have to account for the fact that many formulations contain multiple solids with different densities. And matching density exactly often requires high concentrations of co-solvents or sugars that create other formulation problems. It's useful as a supplementary strategy but rarely sufficient on its own.
I ran into a situation last year where a cosmetic suspension kept separating during stability testing at 45 degrees Celsius. The formulation was fine at room temperature. The issue turned out to be thermal degradation of the xanthan gum network. At elevated temperatures the polysaccharide chains lose their structured conformation and the viscosity drops dramatically. Switching to a modified cellulose gum that's more thermally stable solved the problem completely. The accelerated stability data at 45C for six weeks showed no separation and no change in particle size distribution.
Common Pitfalls to Avoid
Over-milling is a real problem. People assume smaller particles always equal better stability. While reducing particle size does decrease settling velocity, there's a point where further size reduction becomes counterproductive. Ultrafine particles have enormous total surface area. They attract water and other polar molecules strongly through surface interactions. This can actually increase the effective viscosity of the continuous phase in ways that cause thixotropic breakdown during storage. Particles below one micron also tend to form strong cohesive networks through van der Waals forces that lead to hard agglomerates which are nearly impossible to re-disperse. Another frequent mistake is ignoring the impact of manufacturing sequence. Adding your dry powder to a full tank of liquid creates a very different dispersion profile than pre-dispersing in a portion of the liquid and then diluting. High-shear mixing should happen early in the process while the volume is smaller and the energy input per unit volume is higher. Trying to fix poor initial dispersion with additional mixing later is almost never effective. You'll spend more time and energy and still end up with a inferior product compared to doing it right the first time. Storage conditions deserve more attention than they typically get. A suspension that passes shelf stability at room temperature can fail spectacularly under freeze-thaw cycling. Ice crystal formation disrupts the particle network and can cause irreversible aggregation. If your product will experience temperature fluctuations during transport or storage, you need to test for this explicitly. Thermal cycling tests are straightforward and reveal problems that standard accelerated stability studies miss entirely.
The most reliable approach to suspension stability combines multiple strategies rather than relying on a single mechanism. Optimize particle size distribution first. Ensure proper wetting. Use a combination of electrostatic and steric stabilization. Incorporate a rheology modifier that provides yield stress without making the product impractical. Test under realistic storage conditions including temperature variation. This framework won't solve every problem but it addresses the majority of failure modes I've encountered over the years.