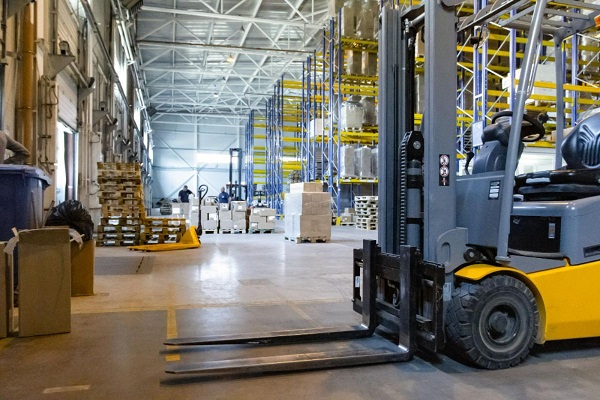
Getting Material Handling Machinery Installed Without Losing Your Mind
I spent about three years dealing with conveyor and forklift track installations across industrial storage facilities in the South Bay. The initial phase is always the same: someone has a floor plan that looks fine on paper, and then you get to the actual building and realize the ceiling height is 4 inches shorter than what the spec sheet said, or there is a sprinkler main running exactly where your motor mount needs to go. This happens constantly in older warehouse structures around San Jose, especially in buildings that were converted from light manufacturing space in the nineties. The real work of Streamlining Storeroom Operations Material Handling Machinery Installations In San Jose starts long before any equipment arrives on site. It starts with documenting what you actually have in the building, not what the blueprints claim you have. I learned that the hard way on a project out near Berryessa where we had ordered a custom overhead monorail system based on as-built drawings from 1998. When we cut the first mounting hole, we hit a structural steel beam that was not on any drawing. The beam was there because someone had reinforced the floor after a forklift accident in 2003. The beam shifted the entire rail alignment by nearly six inches. We ended up modifying three support brackets on site instead of reinstalling the whole system, which would have set us back two weeks and cost roughly eighteen thousand dollars in labor and delays.
Streamlining Storeroom Operations Material Handling Machinery Installations In San Jose
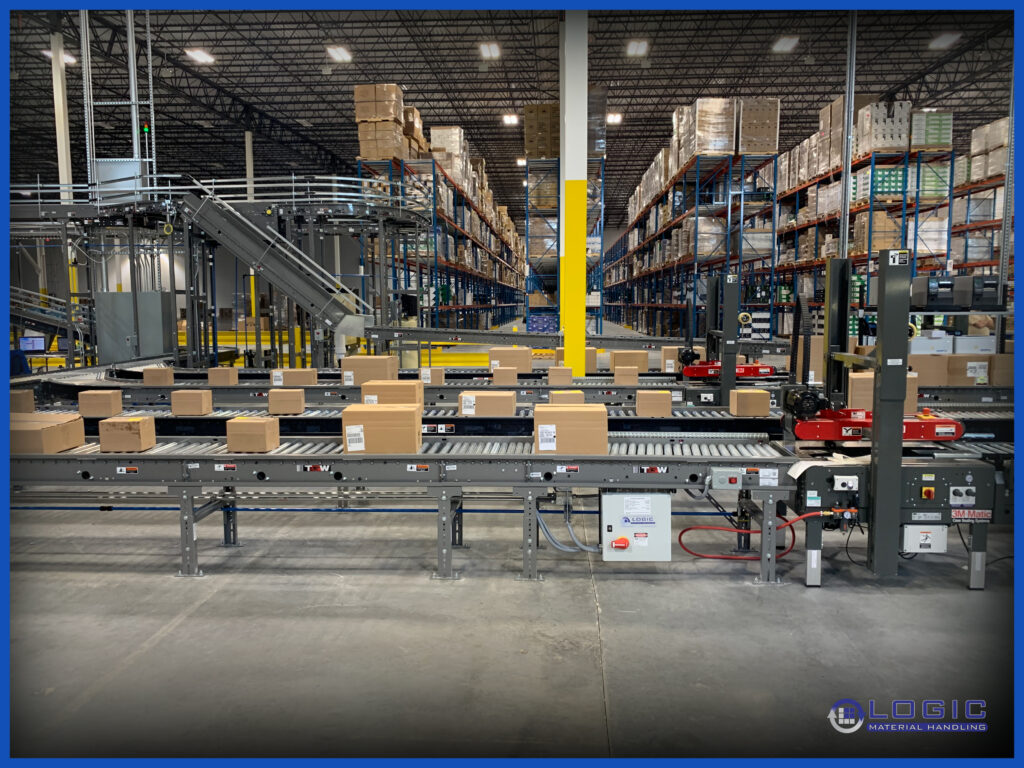
Here is the practical sequence I use now, and it has cut my average install time from about forty hours down to roughly twenty-two hours per standard job. Phase one: pre-site verification. Do not rely solely on existing documentation. Take a laser distance meter and a thermal imaging camera to the site. The thermal camera catches things that standard surveys miss, like hidden ductwork behind dropped ceilings or areas where structural concrete has spalled from water intrusion underneath the floor surface. I have walked into three separate jobs where the floor load rating on paper was seven hundred fifty pounds per square foot, but the thermal scan showed moisture damage in two zones that reduced the effective capacity to about four hundred pounds per square foot. Pouring a concrete pad for a heavy roller conveyor on compromised substrate is a guaranteed failure within eighteen months. Phase two: modular planning. Break the machinery into modules that can be pre-assembled off-site. A standard twenty-foot section of chain conveyor with motors and guards attached in a workshop takes about six hours to assemble correctly. Doing that same assembly on the warehouse floor, with temperature swings and workers tripping over materials, takes closer to twelve hours and the quality is worse. Pre-assembly also lets you run power and control wiring before the unit ever hits the floor. You are not chasing extension cords around an active storeroom.
Phase three: anchored positioning. Use laser trackers or at minimum a high-quality rotary laser level to establish your reference lines. Do not eyeball alignment. I have seen installations where the conveyor was off by a quarter inch over a forty-foot run, and that small error compounded at each transfer point until product started binding and jamming every forty minutes. The correction cost was two days of downtime and replacing three drive chains. Phase four: utility tie-in. Coordinate with the electrical contractor before the machinery arrives. The most common bottleneck I see is the machine sitting on its pads while waiting for a single twenty Amp circuit to be terminated. In the San Jose area, permitting for new electrical runs in commercial spaces can take between ten and twenty-five business days depending on the jurisdiction. Plan for that. Call the county inspector early if you are in Santa Clara County unincorporated areas. They are reasonable but they do not expedite things on their own. Phase five: commissioning. Run each module empty for at least thirty minutes before loading it with product. Listen for unusual bearing noise, check motor amperage against the nameplate rating, and verify that all safety interlocks function. I once skipped the empty run on a weekend because the project manager was pushing for Monday launch. The drive gearbox failed on Tuesday afternoon during a peak inventory pull. The repair required a full gearbox replacement and four hundred dollars in parts plus two days of labor. The empty run would have caught the misalignment that caused it, and it would have taken twenty minutes.
Get the Full Details

Counter-Intuitive Details Most People Miss
One thing that surprises beginners is that floor-leveling compound is often a worse solution than it appears. When you pour a leveling bed under heavy machinery feet, the compound cures to a rigid plane, but the underlying concrete slab can still shift minimally from temperature changes and forklift vibration. That movement transfers into the machinery mounts and creates stress points. A better approach in many cases is to use adjustable leveling feet with locknuts. You set the level, torque the locknuts, and if the building settles or shifts, you relevel rather than break out concrete. It adds about forty-five minutes to the install but saves hours of corrective work later. Another detail: the location of your control panel matters more than most people think. Mounting a VFD or PLC enclosure directly above a conveyor drive creates heat problems. The VFD generates significant thermal output and when you stack it above the motor, you are cooking both components. Place the control panel at least three feet laterally away from the drive motor, and ensure there is cross-ventilation. I used to mount panels directly above drives to save conduit runs. That saved maybe two hours of wiring time and created persistent overheating failures that cost me three weekends of troubleshooting over a six-month period.
Where This Approach Falls Apart
This methodology does not work well in buildings with active operations running around you. If your storeroom is shipping and receiving inventory twenty hours a day, you cannot pre-assemble modules on the floor because you have no clear space, and you cannot shut down power for extended periods because the operation depends on it. In those cases, the only viable path is phased installation during off-hours, which typically increases total labor cost by about thirty percent due to overtime rates and the slower pace of night work. There is no way around that. If your facility runs twenty-four hours, plan accordingly or accept the delay. Another scenario where this breaks down is when the machinery you are installing is significantly heavier than the original building design anticipated. No amount of planning will fix a floor that cannot support the load. If your new roller conveyor system with full loads exceeds the floor capacity, you need structural reinforcement, not better installation tactics. That means engaging a structural engineer, which adds approximately two to three weeks and four to eight thousand dollars to the project before you even unbox a single piece of equipment. If you need a layout template for the pre-assembly phase, I keep a standard spreadsheet that tracks module dimensions, mounting hole patterns, electrical requirements, and clearance zones. It is not fancy but it has saved me from ordering the wrong bolt length at least six times. The key is filling it out before you order anything, not after.