Support Removal on Bambu Printers: What Actually Works
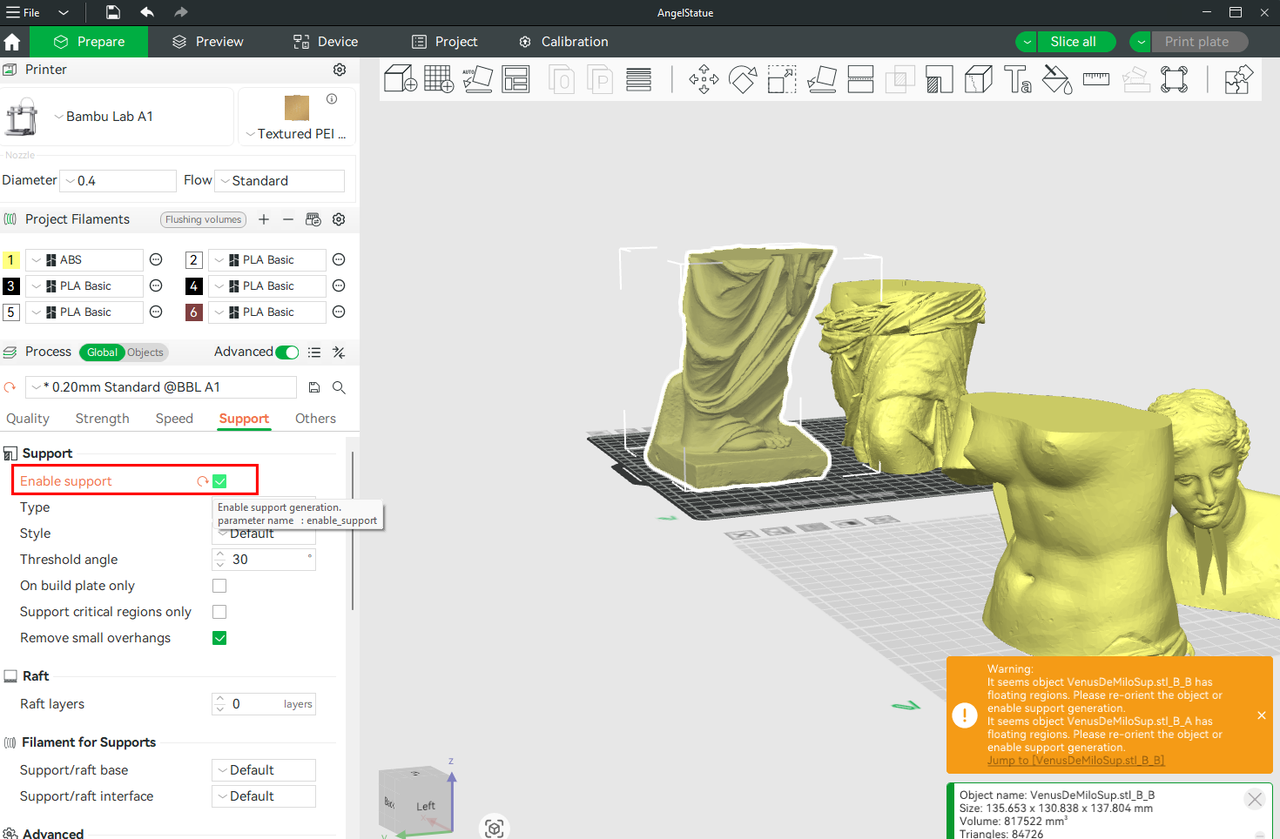
I spent about three weeks debugging why my overhangs kept tearing because I was printing them at a 5-degree angle with normal supports instead of letting the tree support handle it. The supports held the model but the adhesion was so aggressive that removing them shredded the surface. That particular print ended up as scrap. After that I started paying closer attention to how Bambu Studio sets up supports by default and how the interaction between support modifiers, interface layers, and material choice changes the removal process entirely. Bambu Studio handles support generation through several different algorithms, and the default setting is not always the one that makes removal easiest. The software gives you tree supports, normal supports, and a few variants. Tree supports generally remove faster and leave less scar tissue on the print surface. They connect to the model through small touch points instead of broad flat contact areas. Normal supports create a wider contact zone and tend to fuse harder into the bottom layers of your object, especially on materials like PETG where support adhesion runs higher than with PLA. The interface layer is where most people make their first mistake. Bambu Studio calls these "support interface" layers and they sit between the support structure and the actual printed model. The default setting for PLA usually applies two interface layers with the same material and temperature as the main print. Two layers is often enough to make removal clean. Going to zero interface layers can cause the support to bond directly to your model surface, which means you will likely pull fibers or leave pitting when you break the support away. Increasing to three or four layers sometimes helps with very difficult geometries, but it also creates a thick zone that requires scraping after removal. The practical sweet spot for most prints is two interface layers with a slightly reduced temperature, usually three to five degrees lower than the nozzle temperature, to weaken that bond without losing structural integrity.
There is a setting in Bambu Studio called "Wipe support on" that I did not understand for months. It adds extra filament deposition along the bottom edges of support structures to improve contact with the build plate or previous layers. The side effect is that it also makes supports harder to remove from the model because the interface between the support and the object gets reinforced. Turning this off for supports that touch delicate surfaces often makes a noticeable difference. You only lose a small amount of bottom support stability, which rarely matters unless you are printing something extremely tall with a very narrow footprint. PETG support removal is where people get frustrated the fastest. PETG creates a chemical-style bond with itself rather than just a mechanical grip, and the standard support removal technique of snapping the support off leaves rough patches that require significant post-processing. The workaround most people miss is increasing the Z-distance for support interfaces. If you go to Print Settings > Support Material and look at the interface Z distance, bumping that value from the default of 0.10 mm up to 0.12 or even 0.14 mm creates more separation between the support and the model surface. The supports still hold the overhangs properly but come away with much less force and leave a smoother finish. I learned this after spending an afternoon sanding PETG parts that could have been ready in twenty minutes with a different Z-distance setting. Tree supports in Bambu Studio have a parameter called "branch distance" that controls how close the tree branches come to the model surface. The default is usually 0.4 mm, which is fine for most cases but can leave larger touch points on fine details. Reducing this to 0.3 mm gives you smaller contact areas that are easier to snap off cleanly. The trade-off is that the support becomes less rigid and may not hold up well on very wide overhangs greater than 60 degrees. In those cases you need to either add a support modifier block under the overhang or switch back to normal supports for that region only.
Support modifiers are one of those features that beginners overlook because they seem complicated. They let you define a box around a specific part of your model and apply different support settings to that area. If you have a section of your print with complex geometry where normal supports would leave ugly marks, you can place a modifier box there and set it to use tree supports with zero interface layers and a higher Z distance. This gives you targeted control instead of applying the same aggressive support strategy across the entire model. When it comes to removing supports after the print finishes, the tool choice matters more than most people expect. Standard wire cutters work fine for tree supports on PLA prints, but for dense normal support structures a pair of flush cutters or even small nail clippers gives you a cleaner break. The goal is to cut as close to the model surface as possible without actually touching the print. Snipping flush leaves a small nub that sanding or scraping removes quickly. Pulling supports off by hand when they are still warm works too, but only if the material is PLA. PETG and ABS supports need to cool completely before any force is applied, otherwise you risk deforming the underlying geometry. Sanding removed support areas follows a predictable progression. Start with a 400-grit sanding stick or fine emery board to knock down the largest nubs, then move to 800-grit, then 1200-grit if you need a smooth finish. For PLA this usually takes five to ten minutes per part depending on how aggressively the supports were configured. For PETG it takes longer because the material is tougher and more elastic. A sharp hobby knife held at a shallow angle works better than sandpaper on flat surfaces where you want to avoid creating uneven wear patterns. Scrape gently and check your progress frequently. One deep gouge with a knife ruins more prints than careful sanding ever will.
Get the Full Details

Dissolvable supports with PVA or BVOH are an option on Bambu printers, but they require a dual-extrusion setup or a filament swap. The practical limitation is that PVA softens at relatively low temperatures and can become gummy if your humidity is high. I had a print where the PVA support absorbed moisture from the air overnight and turned into a sticky mess inside the support structure instead of dissolving cleanly. Drying the PVA filament in a sealed container with desiccant before use prevents that problem. Even dried PVA can take several hours of water soaking depending on how dense the support structure is, and some internal channels never get fully cleaned without a toothbrush or compressed air. There is a setting in Bambu Studio called "Keep support material from becoming waste" that sounds useful but actually increases support density in places where it is not needed. The option attempts to optimize support volume by leaving thin connection points rather than full support structures. The result is that those thin points become extremely difficult to remove because they fuse into the model surface as the filament cools. I turned this off on a test print and the support removal time dropped by roughly half compared to the optimized version, even though the total support volume was slightly higher. Less support material does not always mean faster post-processing. If you are printing with ASA or ABS and using soluble supports, the removal process involves a different chemical approach. These materials respond better to isopropyl alcohol than to water for dissolving the support structure. Water will eventually work but it takes significantly longer and can warp the outer layers of the printed part. The IPA soak method usually clears supports from complex internal geometries in about one to two hours depending on support density. Agitating the solution occasionally speeds things up, but aggressive stirring can damage delicate features on the model itself.
The most common mistake I see on forums is people complaining about support scarring and then sharing screenshots of their support settings where the interface layers are disabled entirely. Some believe that removing interface layers makes supports easier to take off, but the opposite is usually true. Interface layers are designed to be the sacrificial zone. Without them the support fuses directly to your model's outer shell. Keeping two interface layers and adjusting the Z distance and temperature instead of eliminating them entirely produces cleaner results in almost every material I have tested. Another detail that affects removal speed is the support gap. This is the distance between the support structure and the model surface measured in nozzle diameters. The default of 0.4 mm for a 0.4 mm nozzle works for most PLA prints. Increasing it to 0.6 or 0.8 mm reduces the contact pressure and makes snapping supports away significantly easier. The downside is that very wide gaps can cause overhangs to sag slightly before the support catches them, especially on large flat surfaces. Testing with a single overhang print at different gap values takes about fifteen minutes and tells you more than reading forum posts. Post-processing speed varies by material and support type but here is a realistic range. A PLA print with tree supports and two interface layers usually takes ten to fifteen minutes to fully clean up. The same model with normal supports and zero interface layers on PETG can take forty-five minutes to an hour including sanding. Understanding which combination you are dealing with before you start the print helps you plan accordingly and avoid ending up with a part that looks acceptable but requires hours of finishing work.