Understanding Abrasive Media for Surface Preparation
The grit size you pick determines everything about your blast job. Too coarse and you gouge the substrate. Too fine and you waste an hour watching nothing happen. I have rebuilt enough blast pots and ruined enough workpieces that I can tell you exactly where things go sideways. Sandblasting Grit Sizes Your Comprehensive Guide To Choosing The Right One
What Grit Size Actually Means
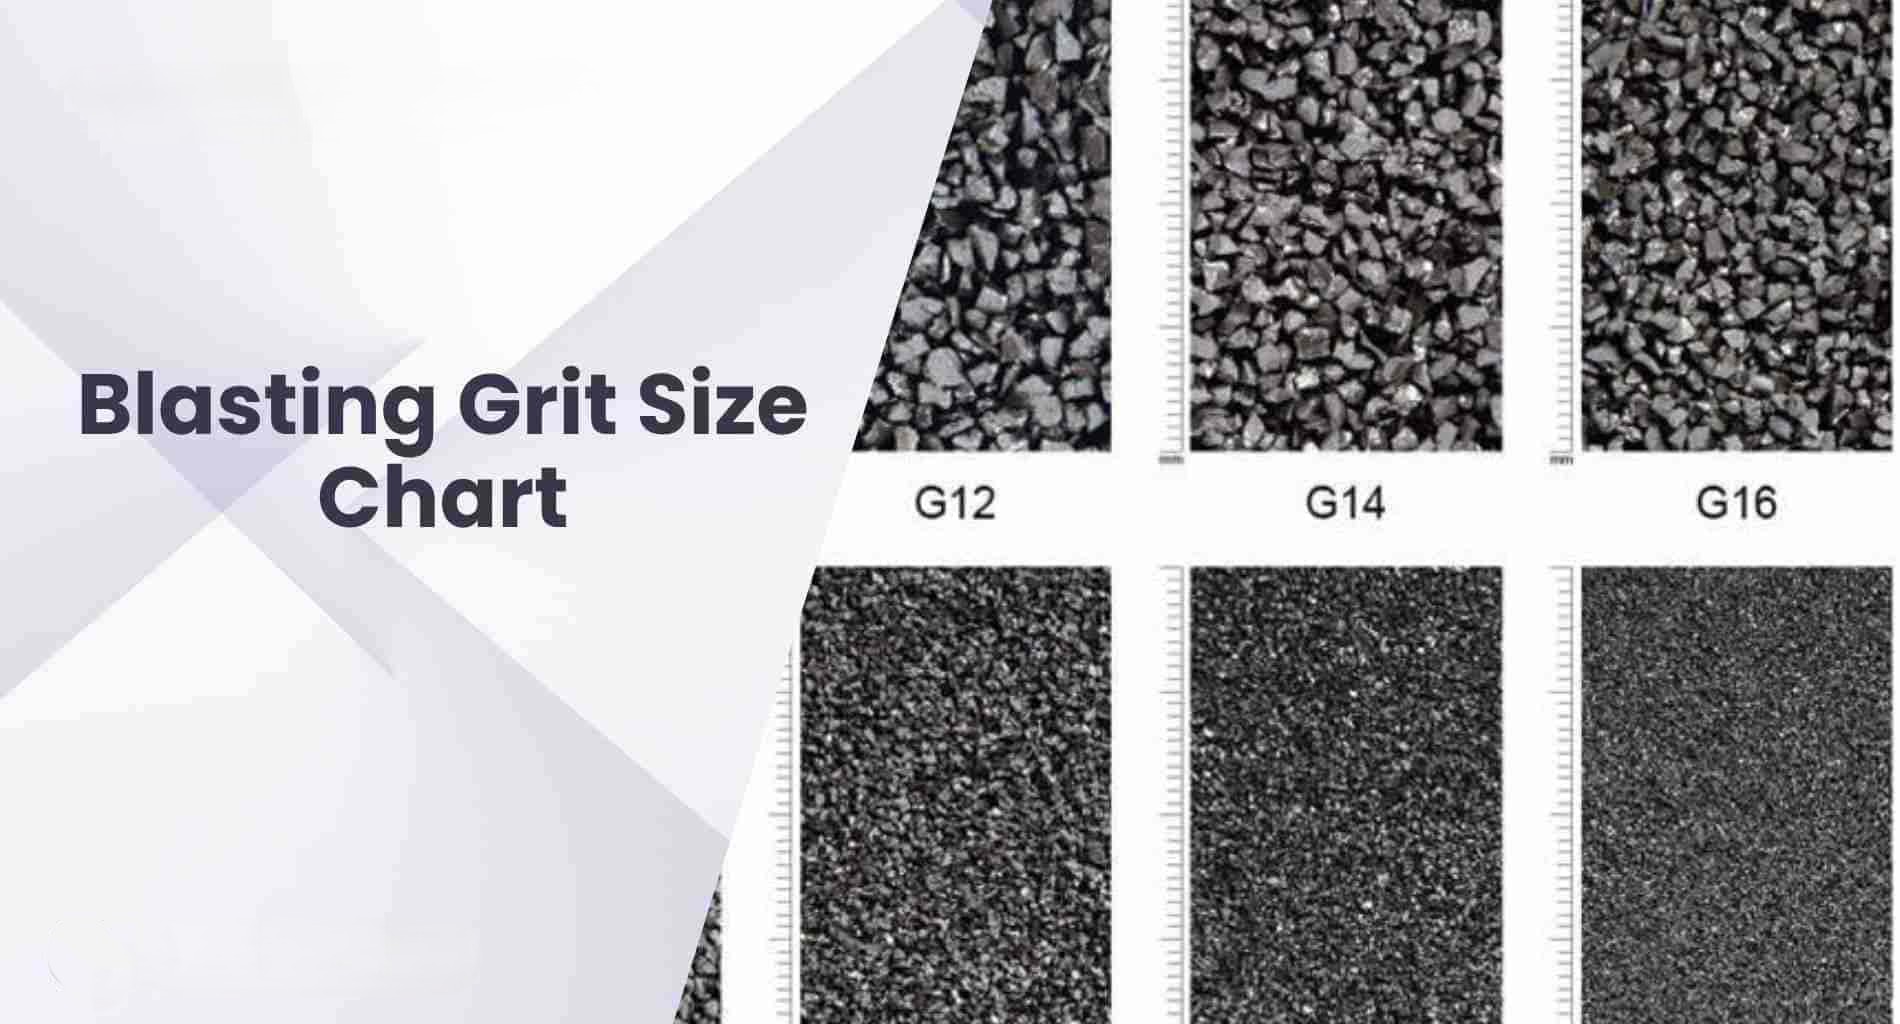
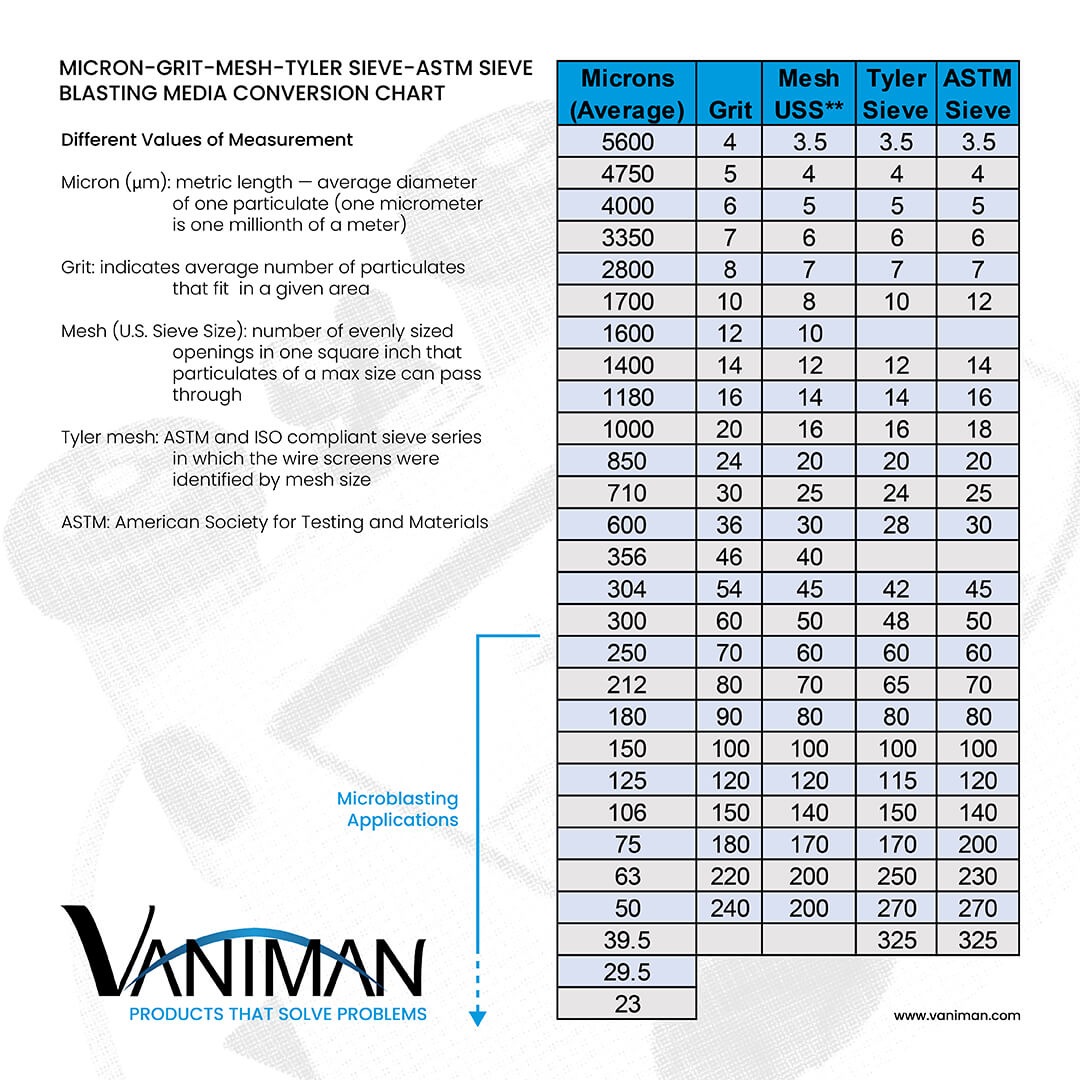
Grit size is measured in mesh count, which refers to the number of openings per linear inch in a screening sieve. A higher mesh number means smaller particles. This is backwards from how most people intuitively think about it. You might assume #100 grit is larger than #40 grit, but it is the opposite. The naming convention comes from wire cloth manufacturing, not from the abrasive itself. I once shipped a customer three tons of Alcoa's aluminum oxide labeled as 40-grit, only to have them call me furious because the media felt like dust. The lot had been regraded and the actual size distribution was closer to 80-grit. This happens more than it should. Always verify incoming media with a sieve analysis before committing to production work. My workaround was setting up a controlled sieve test on every new shipment using a Ro-Tap sieve shaker and a stack of ASTM E11 certified sieves. Takes twenty minutes. Saved me from two potential disaster orders.
The Standard Grit Ranges and What They Do
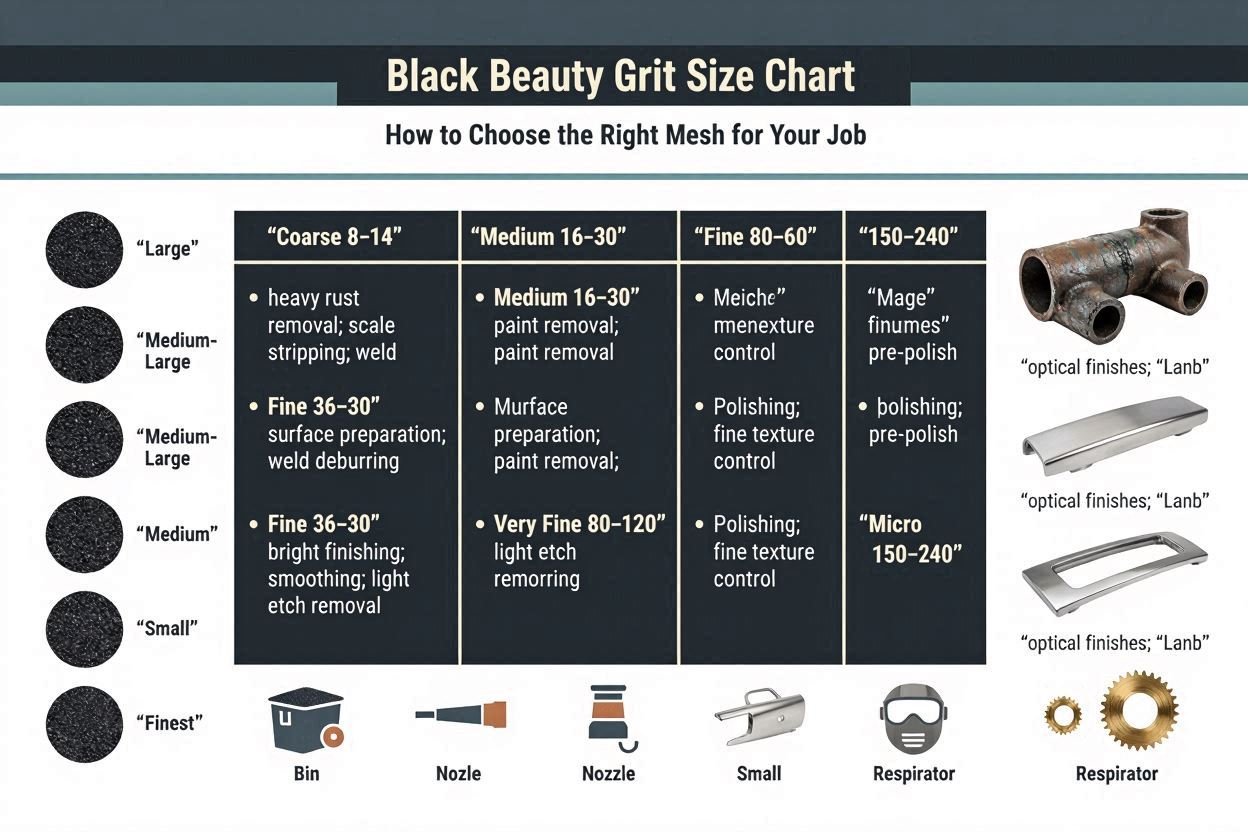
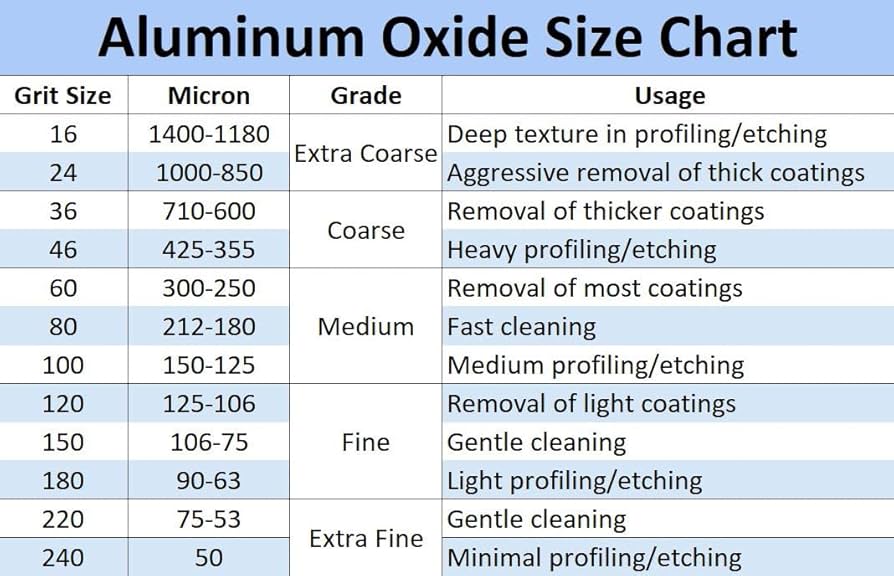
Fine range (100 to 150 mesh): This is where you go for surface profiling before coating, not for paint removal. It produces a clean anchor pattern typically in the 1 to 3 mil range. I use this for preparing aluminum aircraft skins before bonding. It cleans without embedding into the soft base metal. The tradeoff is that it moves slowly. You are looking at roughly 15 to 20 square feet per minute on bare steel when your nozzle is in good condition and pressure is held steady at 90 to 100 PSI. MEDIUM range (20 to 60 mesh): The workhorse zone. 36-grit aluminum oxide or crushed glass sits right here and strips paint, rust, and mill scale at a reasonable rate. This is the default choice for structural steel preparation to SSPC-SP6 or near-white metal finishes. A properly sized 36-grit charge through a 3/8-inch nozzle at 100 PSI will remove coating at maybe 200 to 400 square feet per hour depending on coating thickness and hardness. That is where most production shops live. I keep 40-grit and 50-grit in rotation for general fabrication and reconditioning work. Coarse range (8 to 30 mesh): Used for heavy-duty stripping and fast material removal. I ran into a situation once where a client needed to strip epoxy coating off a 1970s storage tank interior that had built up to over forty mils in places. Standard 36-grit was chewing through media at an unacceptable rate and making no progress. I switched to 16-grit garnet and cut the job time by about sixty percent. Garnet is heavier than aluminum oxide at the same mesh size, so it hits harder on impact. The downside is it leaves a more aggressive profile that may not be suitable if you are applying thin-film coatings afterward.
Get the Full Details
How to Pick the Right Grit for Your Application
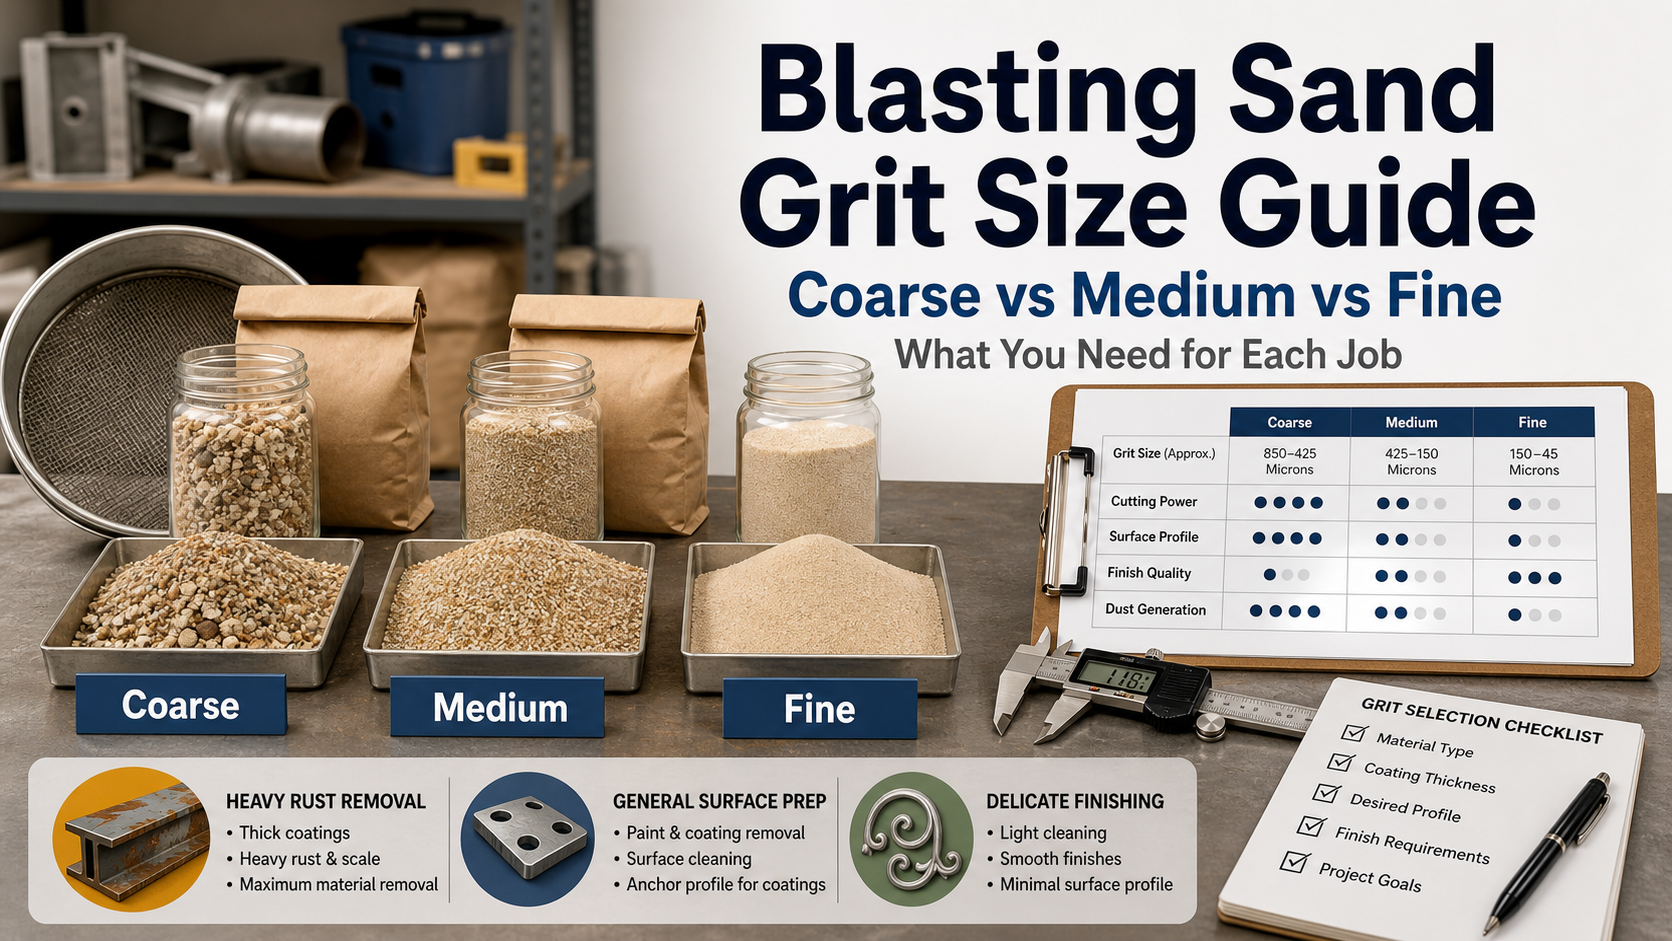
The decision matrix is straightforward once you know what you are trying to accomplish. If you are removing thick coatings from heavy steel, go coarse. If you need a specific surface profile for a coating system, match the grit to that profile requirement. If you are working on thin metal or delicate substrates, go fine and accept the slower rate. Surface profile depth matters more than most people realize. The anchor pattern created by the blast media needs to be compatible with the coating you plan to apply. Most epoxy and polyurethane coatings perform best with a profile of 1.5 to 3 mils. If you profile too aggressively with coarse media on thin gauge steel, you risk burning through the material. I had a job where someone used 20-grit on 16-gauge sheet metal and punctured half the panels. Lesson learned on that one. The hardness of the substrate is another factor nobody talks about enough. Soft metals like aluminum, brass, and copper will deform under aggressive blasting even at fine grits. For those materials, I recommend using a softer abrasive like baking soda or walnut shell at a correspondingly finer size, and keeping the pressure below 40 PSI. The goal is cleaning, not cutting.
Media Type Interacts with Grit Size
Grit size alone does not tell the whole story. The material composition of the abrasive changes how it behaves at any given mesh count. Aluminum oxide is sharp and angular, which makes it cut fast but also wear down quickly. It typically lasts two to three passes before the particles become too dull or fragmented to be effective. Glass bead is spherical and rounds surfaces rather than cutting them. It is used for peening, deburring, and cosmetic finishing. At 50-mesh, glass bead will clean a surface but leave a matte satin finish rather than a profiled one. Crushed glass and garnet sit somewhere between these two. They are angular like aluminum oxide but break down slower and produce less dust. I prefer garnet for outdoor blasting operations where recyclability and dust control matter. It recycles about four to six times before replacement is needed, compared to two to three for aluminum oxide at the same application. Steel shot and steel grit are the heavy hitters for industrial prep work. Steel shot is spherical and produces a dimpled profile ideal for shot peening fatigue life. Steel grit is angular and cuts aggressively. Both come in sized grades that correlate loosely to the mesh system but use different naming conventions. You will see designations like S50, S170, or G40. These numbers indicate the approximate mesh equivalent. S50 shot is roughly 50-mesh size. The key difference from mineral abrasives is that steel media can be recycled dozens of times, which makes it economical for high-volume shop work despite the higher upfront cost.
Common Mistakes That Wreck Projects
The most frequent error I see is mismatching grit size to nozzle condition. A worn 3/8-inch nozzle at 100 PSI will perform like a 5/16-inch nozzle at 70 PSI. Your media consumption drops, your coverage rate drops, and your profile becomes inconsistent. Check your orifice diameter with a go-no-go gauge every shift. Replace the nozzle assembly when you see the barrel walls developing an egg-shaped wear pattern. This is not a theoretical problem. I lost three days on a project because I ignored nozzle wear and couldn't figure out why my production rates were half what they should have been. Another mistake is using the same media across multiple jobs without sorting. Recycled grit carries residue from previous jobs. Old paint chips, rust particulate, and fragmented media all contaminate fresh charges. I set up a vibration screen with 10-mesh and 100-mesh decks on the return line to separate usable media from fines and contaminants. The undersize goes to waste. The oversize gets re-introduced. This simple step extended my media life by about forty percent on recurring jobs. Pressure selection interacts with grit size in ways that are not obvious. Higher pressure does not always mean faster cutting. Beyond about 100 to 110 PSI, you start accelerating the media so fast that it fragments on impact rather than cutting. The energy goes into breaking the grit instead of removing the coating. I measured this directly once with a particle size analyzer at the outlet of a blast hose. At 120 PSI, my 36-grit aluminum oxide had broken down to an average particle size equivalent to 60-grit. Doubling the pressure had accidentally halved my effective grit size. Running at 80 to 90 PSI gave me better cutting performance with less media consumption.

Dust Control and Health Considerations
Fine grits create fine dust. That dust contains silicates, heavy metals from old coatings, and respirable crystalline silica if you are blasting concrete or stone. OSHA's permissible exposure limit for respirable crystalline silica is 50 micrograms per cubic meter averaged over an eight-hour shift. Wet blasting reduces dust dramatically but changes the media dynamics and requires post-blast drying. Dry blast with a properly filtered recovery system is the cleaner option when configured correctly. I always run a calibrated dust monitor during jobs involving unknown coatings or substrates. The readings tell you whether your ventilation is adequate or whether you need to switch to a different media or method. There is no substitute for actual measurements. Guessing has gotten people sick and companies sued.
Quick Reference for Common Uses
100 to 120 mesh aluminum oxide for cleaning and light profiling on aluminum and stainless steel prior to coating or bonding. Expect about 1 to 2 mil profile depth. 36 to 50 mesh aluminum oxide or garnet for general steel preparation, paint and rust removal, and coating profile development to 2 to 4 mils. This is the default for most industrial maintenance work. 16 to 24 mesh garnet for heavy coating removal on thick steel sections where faster cutting is needed and the aggressive profile is acceptable for the subsequent coating system.
80 to 100 mesh glass bead for peening, stress relief, and cosmetic finishing where a uniform matte appearance is desired without significant material removal. Baking soda at 50 to 80 mesh for sensitive surfaces where media embedding would be catastrophic, such as removing carbon buildup from engine components or cleaning historical masonry without damaging the substrate. The right choice depends on your substrate, your coating system requirements, your production timeline, and your equipment capabilities. Measure your results. Track your media consumption. Adjust based on what the surface actually shows, not what the label on the bag says.