Understanding How CVD Diamond Coating Actually Works On Production Parts
Diamond coating technology has moved from academic labs into real manufacturing over the last decade. The process most people use is chemical vapor deposition, where hydrocarbon gases are broken down at high temperature onto a substrate. The carbon atoms arrange themselves into a diamond cubic lattice. It sounds simple on paper. Getting it right on actual parts is where most people hit problems.
Revolutionizing Material Science Unveiling The Secrets Of Diamondcoating Technology
Before I get into the how-to, I want to address the deposition method because that determines everything else. There are two main approaches for industrial diamond coating: hot filament CVD and microwave plasma CVD. Hot filament uses a tungsten or tantalum wire heated to around 2000°C to crack the gas mixture. Microwave plasma uses a microwave source to generate plasma above the substrate. Each has tradeoffs that matter more than the marketing materials suggest. Hot filament systems are cheaper to build and maintain. You can operate them at pressures between 20 and 100 torr. The downside is that filament contamination is a real issue. Tungsten deposits into your coating if the filament degrades, and that introduces graphitic carbon and weakens the layer. I learned this the hard way on a batch of cutting tool inserts I coated for a machining shop. We were running a standard hydrogen-methane mixture at 6% methane concentration, 75 torr, with a filament temperature around 1950°C. After about 40 hours of cumulative runtime, the tungsten cross-contamination started showing up in the XRF readings. The diamond phase purity dropped from about 92% to 78%. The coating looked fine visually. Nobody noticed until we ran ball-on-disk wear tests and saw the coefficient of friction spike from 0.12 to 0.34 against a steel counterpart. The workaround was straightforward but annoying. I switched to a molybdenum filament. It runs hotter, maybe 2100°C, and the vapor pressure is lower, so contamination drops significantly. The tradeoff is filament lifetime goes from roughly 60 hours down to about 20 hours on this particular geometry. You factor that into your cost model. Molybdenum filaments cost more upfront but the coating yield was higher because we weren't throwing away contaminated batches. That mattered more than the filament replacement frequency.
Substrate Preparation: The Step Everyone Skips or Rushes
The biggest failure mode in diamond coating isn't the deposition itself. It's substrate preparation. Diamond nucleation on non-diamond surfaces requires active sites. Most commercial protocols use diamond grit slurry polishing followed by ultrasonic cleaning. But the grit size, the polishing time, and the cleaning solvent all interact in ways that aren't obvious until you're debugging a coating that won't stick. For tungsten carbide substrates, which are common in cutting tool applications, I recommend a two-stage diamond slurry process. Start with 7-micron grit for about 15 minutes in an ultrasonic bath with isopropanol. Then switch to 1-micron grit for another 10 minutes. Rinse with fresh isopropanol and dry under a nitrogen stream. The key insight is that the larger grit creates deep scratches that act as nucleation wells, but the finer grit after that fills in the valleys and leaves a uniform distribution of active sites. If you skip the second stage or reverse the order, you get patchy nucleation. Some areas will have dense diamond grains while others stay bare. That unevenness leads to stress concentration points during service, and the coating delaminates prematurely. I ran into this on a set of drill bits we were coating for a company doing deep-hole drilling in Inconel. The parts came back from the coater with beautiful diamond coverage under optical microscopy. They looked perfect. But when the operators started drilling, the coating spalled off within the first five holes. The problem was that the nucleation density was too low in certain zones because the grit polishing had been done inconsistently across the batch. The coater had used a single 3-micron slurry step instead of the two-stage approach. After we re-prepared a second batch with the proper sequence and re-coated, the drill bits lasted 40 times longer than uncoated equivalents. That's not a theoretical improvement. We measured it on the shop floor.
Deposition Parameters That Actually Matter
There are a dozen parameters you can tweak during CVD diamond coating. Most people focus on temperature and gas flow rates because those are the easy ones to adjust. But pressure, methane concentration, and substrate bias are just as important and often overlooked. Substrate temperature typically runs between 750°C and 950°C for high-quality diamond films. Below 750°C, you tend to get more graphitic phase mixed in. Above 950°C, the growth rate drops off because the surface re-etching by atomic hydrogen starts outpacing the carbon deposition. The sweet spot depends on your gas mixture and pressure, but 800 to 870°C is a good starting range for most setups. Methane concentration in the hydrogen feed gas is critical. The standard ratio is between 1% and 10% CH4 in H2. Lower concentrations favor diamond growth over graphitic carbon. Higher concentrations increase the deposition rate but also increase the probability of non-diamond carbon forming. I've seen operators crank the methane up to 15% trying to speed things along. The coatings come out faster but they're softer and more prone to cracking. The Vickers hardness drops from around 80 GPa to maybe 40 GPa. That's a meaningful difference when you're trying to protect a cutting edge.
Get the Full Details

Substrate bias is another parameter that deserves more attention. Applying a negative DC bias to the substrate during deposition can improve adhesion and densify the film. But too much bias causes ion bombardment damage. I typically run between -50 and -100 volts for carbide substrates. Going below -150V starts to degrade the coating quality noticeably. The ion energy needs to be high enough to activate surface mobility but low enough that you're not sputtering away the diamond you just deposited.
Post-Processing and Quality Control
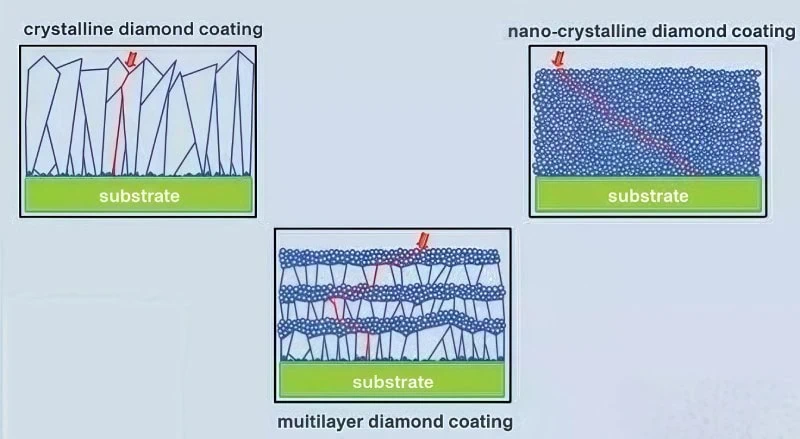
After the coating runs, you need to characterize it properly. Raman spectroscopy is the standard tool for checking diamond phase purity. The diamond peak sits at about 1332 cm^-1. A broad peak around 1580 cm^-1 indicates graphitic carbon. A clean spectrum with a strong 1332 cm^-1 peak and minimal background tells you you've got good diamond content. But Raman alone doesn't tell the whole story. Scanning electron microscopy gives you grain size and morphology information. Typical CVD diamond coatings have grain sizes between 0.5 and 5 microns for fine-grained films. Larger grains give smoother surfaces but can expose sharp grain boundaries that become crack initiation points. For cutting tool applications, a fine-grained coating around 1 micron average grain size tends to perform best. The hard, dense structure resists abrasive wear better than a coarse-grained alternative. X-ray diffraction can confirm the cubic diamond structure and detect any trace phases. Indentation testing measures adhesion strength. I use a standard scratch test with a Rockwell C indenter. The critical load where the coating first delaminates tells you your adhesion quality. Good diamond coatings on properly prepared carbide should handle critical loads above 40 newtons. Below that, something went wrong with the preparation or the deposition parameters.
Limitations You Need to Accept
Diamond coating is not a universal solution. It has real limitations that people gloss over in promotional material. The first issue is temperature. Diamond oxidizes in air at temperatures above about 700°C. So if your application involves sustained high-temperature exposure, the coating will degrade. A PVD aluminum nitride coating might be a better choice for tools that see those kinds of temperatures, even though it's not as hard. Another limitation is the coefficient of thermal expansion mismatch between diamond and many substrates. Diamond has a very low CTE, around 1 ppm/K. Tungsten carbide is closer to 4.5 ppm/K. That difference creates residual stress in the coating during cooling from deposition temperature. The stress is compressive, which is actually beneficial for hardness, but it can also lead to buckling or delamination if the coating is too thick. Most practical diamond coatings are between 5 and 20 microns thick. Going beyond that increases the risk of spalling without proportional benefit. Iron and cobalt are catalysts for diamond graphitization. If your substrate contains free iron or cobalt, or if you're using a binder phase that outgasses those elements during deposition, the diamond quality near the interface suffers. Some people address this with a diffusion barrier layer, usually a thin deposit of titanium or chromium applied before the diamond coating. I've found that a 0.5-micron chromium underlayer helps significantly on cobalt-bonded cemented carbide. The chromium forms a stable carbide layer that prevents carbon solubility issues at the interface.

Cost is another practical constraint. A typical CVD diamond coating run on a set of end mills takes about 8 to 12 hours. The equipment depreciation, gas costs, and labor add up. You're looking at maybe $200 to $500 per tool depending on size and geometry. Whether that's worth it depends on the application. For high-volume production machining where tool changes cost more in downtime than the coating itself, it pays for itself quickly. For one-off prototyping work, you might be better off with a different coating strategy or a different tool material entirely.
Practical Walkthrough for a Small Batch Run
Here's how I'd approach coating a batch of ten indexable insert holders for a milling operation. Load the inserts onto a rotating carousel that keeps all surfaces exposed to the plasma. Rotate at about 5 RPM so each face gets uniform exposure. Place the carousel in the deposition chamber and pump down to below 10 torr base pressure. Backfill with hydrogen to 60 torr. Ignite the microwave plasma at 2.45 GHz and bring the substrate temperature to 850°C over about 30 minutes. Once at temperature, introduce methane to reach a 4% concentration. Run the deposition for 6 hours. That gives you roughly a 10-micron coating at a typical growth rate of 1.5 to 2 microns per hour for these conditions. After the run, let the chamber cool under hydrogen flow to prevent oxidation of the coating surface. When the temperature drops below 200°C, vent the chamber and inspect the parts. Run Raman spot checks on three random inserts. Check the SEM cross-section on one insert to verify coating thickness and grain structure. Do a scratch test on a sacrificial insert to confirm adhesion. If everything passes, the batch is good. The whole process from loading to final inspection takes about 10 hours including cool-down. That's the timeline you're working with for a single coating cycle. The diamond coating field moves fast. New substrate pretreatment methods, alternative gas chemistries, and pulsed plasma techniques are being published regularly. The fundamentals don't change much though. Nucleation matters more than growth rate. Substrate preparation is where most failures originate. And no coating is perfect for every application. Understanding where the technology breaks down is just as important as understanding where it works well.