
So You Want to Understand How Polymers Actually Form
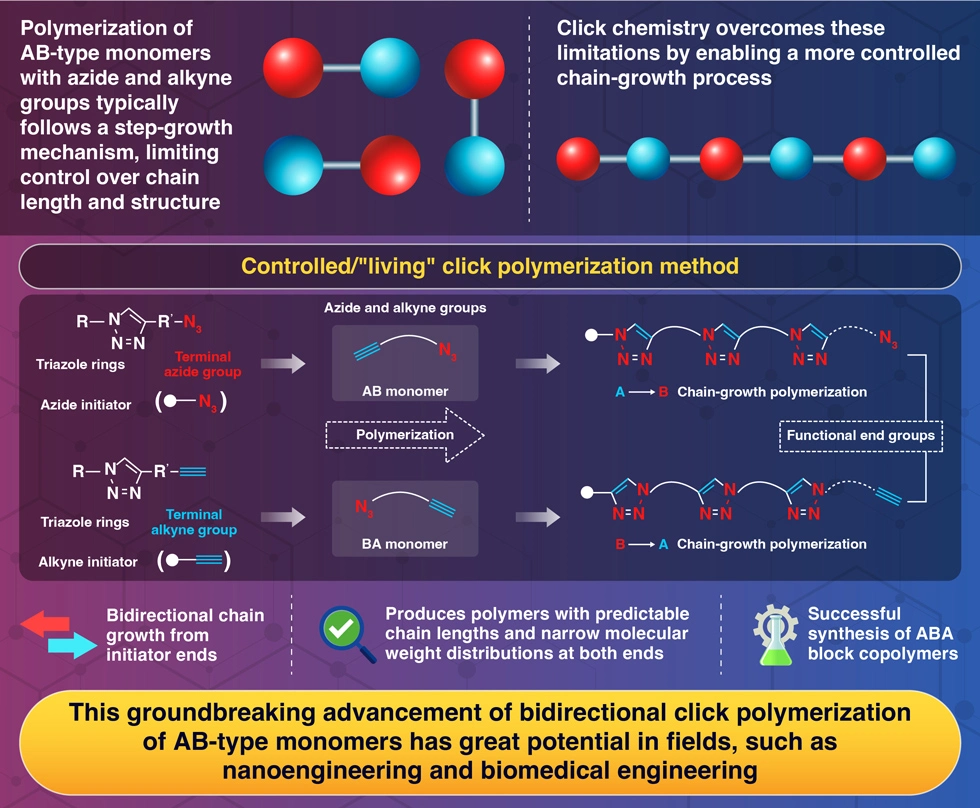
Polymerization is the process where small molecules called monomers link together to form long chains or networks. That is the textbook definition. In practice, it is a lot messier than that. I have spent years working with polymer systems in both research and production environments, and the gap between what the textbooks say and what actually happens in a reactor is significant. Let me walk you through how this works and what you need to know if you are dealing with it for real. There are two main categories you will encounter: addition polymerization and condensation polymerization. Addition polymerization involves monomers with double bonds, typically alkenes, that open up and link together without losing any atoms. Think ethylene becoming polyethylene. Condensation polymerization involves monomers with functional groups that react and release a small molecule, usually water or methanol, as a byproduct. Nylon and polyester come from this route. But the real distinction that matters in practice is between chain-growth and step-growth mechanisms. These do not map perfectly onto addition versus condensation, which trips people up constantly. In chain-growth polymerization, you have an active center — a radical, a cation, or an anion — that adds monomers one at a time to a growing chain. The chains grow fast and reach high molecular weight early in the reaction. In step-growth polymerization, any two molecules with reactive end groups can combine. Dimers react with dimers, trimers react with oligomers, and the molecular weight builds slowly over the course of the reaction. This difference matters enormously for process design.
I ran into this firsthand when I was troubleshooting a polycarbonate production batch that kept coming out with inconsistent viscosity. The specifications called for a narrow molecular weight distribution, but we were getting broad spreads that made the material unpredictable in processing. The issue traced back to moisture contamination in the bisphenol A feedstock. Even parts per million levels of water consume the phosgene and shift the stoichiometry in interfacial polymerization. We ended up installing a molecular sieve drying system on the feed lines and reducing the batch residence time variation from about forty minutes down to under eight. The molecular weight distribution narrowed significantly after that.
The Mechanics of Chain-Growth Polymerization
Chain-growth polymerization proceeds through three fundamental stages: initiation, propagation, and termination. In radical polymerization, which is the most common industrial variant, an initiator molecule breaks apart under heat or light to form free radicals. These radicals attack the double bond of a monomer, creating a new radical on the added monomer unit. This new radical then reacts with another monomer, and the chain grows rapidly. Termination occurs when two growing chains meet and combine or disproportionate, ending the active center. The kinetics here are governed by the rates of these individual steps. The overall polymerization rate depends on the square root of the initiator concentration in ideal cases. That means doubling your initiator does not double your rate — it increases it by about forty percent. Molecular weight, on the other hand, tends to decrease as initiator concentration increases because more chains are growing simultaneously from more active centers. This inverse relationship between rate and molecular weight is one of the central trade-offs in polymer synthesis. Living polymerization techniques, particularly atom transfer radical polymerization and reversible addition-fragmentation chain transfer, have changed this landscape considerably. These methods suppress termination by maintaining a dynamic equilibrium between active and dormant species. The result is polymers with controlled molecular weights and very narrow polydispersity indices, sometimes below 1.1. This is critical when you need consistent mechanical properties across batches. The downside is that living systems are more sensitive to oxygen and impurities, and they typically require longer reaction times. A standard free radical polymerization of methyl methacrylate might take two to four hours at eighty degrees Celsius. A controlled radical version could take six to twelve hours under similar conditions.
Get the Full Details

Step-Growth Polymerization and Its Quirks
Step-growth polymerization follows completely different kinetics. The Carothers equation describes the relationship between conversion and degree of polymerization. You need extremely high conversion — typically above ninety-eight percent — to achieve high molecular weight. At ninety-five percent conversion, your average chain length is only about twenty units. Push to ninety-nine percent and you get roughly one hundred units. This is why closing the reactor tightly and removing the condensation byproduct efficiently is so important in condensation polymerizations. Vinyl polymers dominate the commercial landscape, but engineering polymers like polyamides, polyesters, and polycarbonates rely heavily on step-growth mechanisms. These materials generally have higher melting points and better chemical resistance than their vinyl counterparts, which is why they are used in automotive and aerospace applications. The trade-off is that processing them requires higher temperatures and more precise control over stoichiometry. Even a one percent deviation from perfect balance in functional group ratios can cut the achievable molecular weight in half. I once worked on a project involving polyetheretherketone, or PEEK, synthesized through nucleophilic substitution polymerization. The reaction requires aromatic difluoride and hydroquinone monomers in a polar aprotic solvent with a base. The challenge was that the product precipitates out of solution as it forms, which can cause severe mixing and heat transfer problems in scale-up. Our lab-scale batches worked fine in two-hundred-milliliter reactors, but when we moved to a ten-liter pilot reactor, the viscosity climbed so fast that the agitator motor tripped on overload. We solved it by running the reaction at higher temperature and lower solid concentration, then precipitating the polymer afterward. It added a step but saved the batch. The molecular weight dropped by about fifteen percent compared to lab results, but it was still within spec for the target application.
Copolymerization and Structure Control
When you use more than one monomer, you get a copolymer, and the arrangement of those monomers along the chain determines many of the material properties. Alternating copolymers have monomers arranged in a strict ABAB pattern. Random copolymers have no particular order. Block copolymers have long sequences of one monomer followed by long sequences of another. Graft copolymers have branches of one monomer type growing from a backbone of another. The reactivity ratios of the monomers determine whether you get random or alternating arrangements in free radical copolymerization. If both reactivity ratios are close to one, the copolymer composition mirrors the feed composition and is essentially random. If one monomer prefers to add to itself and the other prefers to add to the different monomer, you can get blocky or alternating structures depending on the values. This is something you have to calculate before you start, not after you analyze the product. I had a situation where we were making a styrene-acrylonitrile copolymer and the AN content varied between batches despite keeping the feed ratio constant. The issue was that acrylonitrile has a significantly different volatility than styrene, and as the reaction progressed and temperature rose, the vapor composition shifted. We ended up using a semi-batch process where we fed the acrylonitrile gradually over the course of the reaction rather than loading it all at the beginning. This kept the instantaneous feed ratio more constant and brought the AN content variation down from about four percent relative standard deviation to under one percent.
Polymerization Reactor Design and Process Control
The choice of reactor type has a major impact on the quality of the polymer produced. Batch reactors are simple but produce the widest molecular weight distributions because all chains start growing at different times and compete for monomer over varying durations. Continuous stirred-tank reactors, or CSTRs, give narrower distributions but still broader than what you get in a plug flow reactor. For the tightest control, you might use a series of CSTRs in cascade or a tubular plug flow reactor. Heat management is perhaps the most critical engineering challenge in polymerization. The reactions are highly exothermic. Styrene polymerization releases about eighty kilojoules per mole. For a large batch reactor producing several tons of polystyrene, the total heat output can exceed several megawatts during the peak reaction rate. If that heat is not removed quickly enough, the temperature runs away, the reaction accelerates further, and you can end up with degraded polymer or even a dangerous pressure buildup. Jacketed reactors with careful temperature profiling are standard, but for very exothermic systems, you might need internal cooling coils or a two-phase cooling medium. Monomer conversion also affects viscosity dramatically, which in turn affects heat transfer and mixing. Early in a polymerization, the mixture behaves like a low-viscosity liquid. As chains grow and concentration increases, you can see viscosity climb by orders of magnitude. In bulk polymerization of MMA, for example, the viscosity might go from about 0.9 centipoise for pure monomer to over a thousand pascal-seconds near complete conversion. This is thick enough that agitation becomes ineffective and heat transfer through the bulk is severely limited. That is why many industrial processes use solution or suspension polymerization to keep the viscosity manageable.
Common Pitfalls and What They Look Like in Practice
Oxygen inhibition is a well-known problem in radical polymerization. Molecular oxygen reacts with free radicals to form relatively stable peroxy radicals that do not initiate polymerization effectively. In open systems or poorly degassed setups, you can get a thin layer of unpolymerized material on the surface even when the bulk has fully cured. This is particularly annoying in coating applications. The standard workaround is to purge with nitrogen or argon before starting the reaction, or to use monomers like acrylates that can react with peroxy radicals to regenerate active species, though this is less reliable at larger scale. Poisoning of catalysts in coordination polymerization, such as Ziegler-Natta or metallocene systems, is another frequent issue. These catalysts are extraordinarily sensitive to impurities like water, oxygen, sulfur compounds, and even certain metals. Parts per billion levels can kill activity. Feedstocks that are perfectly acceptable for free radical polymerization can completely deactivate a metallocene catalyst. I spent an entire week chasing down a mysterious loss of activity in a propylene polymerization run before we traced it to a contaminated gasket material in the feed line. The elastomer was leaching sulfur-containing additives into the monomer stream at concentrations far below what you would typically test for. Gel effect, or Trommsdorff effect, is another phenomenon that catches people off guard. As conversion increases and viscosity rises, the diffusion of growing radical chains becomes restricted. Termination reactions, which require two large chains to find each other, slow down much more than propagation, which involves a small monomer adding to a chain end. The net result is an auto-acceleration of the polymerization rate and a spike in molecular weight. This can be beneficial in some cases, giving you higher molecular weight at moderate conversion, but it can also lead to hot spots and runaway in poorly controlled systems. The effect is most pronounced in bulk and solution polymerizations at conversions above about twenty percent.
Characterization and Quality Control
Gel permeation chromatography, or GPC, is the standard method for determining molecular weight distribution. It separates polymer chains by size as they pass through a porous column. The elution volume correlates with hydrodynamic volume, which you convert to molecular weight using polystyrene standards. This works well for comparative purposes, but remember that the absolute molecular weights are only accurate for polystyrene. Different polymer architectures and chemistries have different relationships between hydrodynamic volume and actual molecular weight. If you need absolute values, you should couple GPC with light scattering or viscometry detectors. Differential scanning calorimetry gives you the glass transition temperature and melting behavior, which are essential for understanding how the polymer will perform in service. A single glass transition indicates a homogeneous material. Multiple transitions suggest phase separation, which is common in block copolymers and polymer blends. The position and width of the glass transition can also tell you about chain mobility, crosslink density, and residual solvent content. Thermogravimetric analysis shows you the thermal stability and decomposition profile. Most vinyl polymers begin to degrade above three hundred degrees Celsius through random chain scission. Polyacrylates tend to depolymerize back to monomer at high temperatures, a process called unzipping. Condensation polymers often decompose through side reactions rather than simple bond cleavage. This information is important for processing — if you are extruding or injection molding at elevated temperatures, you need to stay well below the degradation threshold while still achieving sufficient fluidity.
What This Means for Material Selection
Understanding the polymerization mechanism helps you predict and control material properties, but it is only one piece of the puzzle. The same polymer made by different methods can have significantly different properties. High-density polyethylene produced with a Ziegler-Natta catalyst has a different branching structure and crystallinity than one produced with a metallocene catalyst, even though both are technically HDPE. The metallocene version can achieve narrower molecular weight distribution and more uniform comonomer incorporation, which translates to better environmental stress crack resistance and optical clarity. Crosslinking is another factor that polymerization chemistry determines. Thermosets like epoxies and polyurethanes form three-dimensional networks that cannot be melted or dissolved once cured. The crosslink density, controlled by the ratio of functional groups and the cure conditions, determines hardness, chemical resistance, and thermal stability. Too few crosslinks and the material is soft and soluble. Too many and it becomes brittle. Finding the right balance requires understanding both the chemistry and the processing constraints. Biodegradable polymers like polylactic acid and polyhydroxyalkanoates are an area of active development. PLA is produced by ring-opening polymerization of lactide, a cyclic dimer of lactic acid. The molecular weight is limited by the equilibrium nature of the reaction and the sensitivity to moisture. Achieving molecular weights high enough for structural applications requires careful removal of water and careful control of the catalyst system. I worked with a lab that was struggling to get consistent results because their vacuum line had a small leak that introduced trace moisture over weekends when nobody was monitoring the system. The molecular weight would drop unpredictably every Monday morning. Installing a proper drying tube and switching to a sealed inert gas blanket solved the problem entirely.
The Bottom Line
Polymerization is deceptively complex. The basic chemistry is straightforward, but controlling it at scale requires attention to kinetics, thermodynamics, heat transfer, mass transfer, and impurity management. The difference between a good polymer and a great one often comes down to details that are easy to overlook — a contaminated feed line, a slightly off stoichiometric ratio, inadequate degassing, or insufficient mixing as viscosity climbs. The people who understand these factors tend to get better results consistently. The ones who do not waste a lot of time and material troubleshooting problems that had simple causes.


